Used CNC Lathes & Turning Centers for Sale
23 results

Haas DS 30Y
USA

Van CNC MR20-V7 Swiss Type Lathe
Mexico

Van CNC MR38-V7 Swiss Type Lathe
Mexico

Van CNC MR38-V7 Swiss Type Lathe
Mexico

Van CNC SM20-V8 Swiss Type Lathe - NEW
Mexico
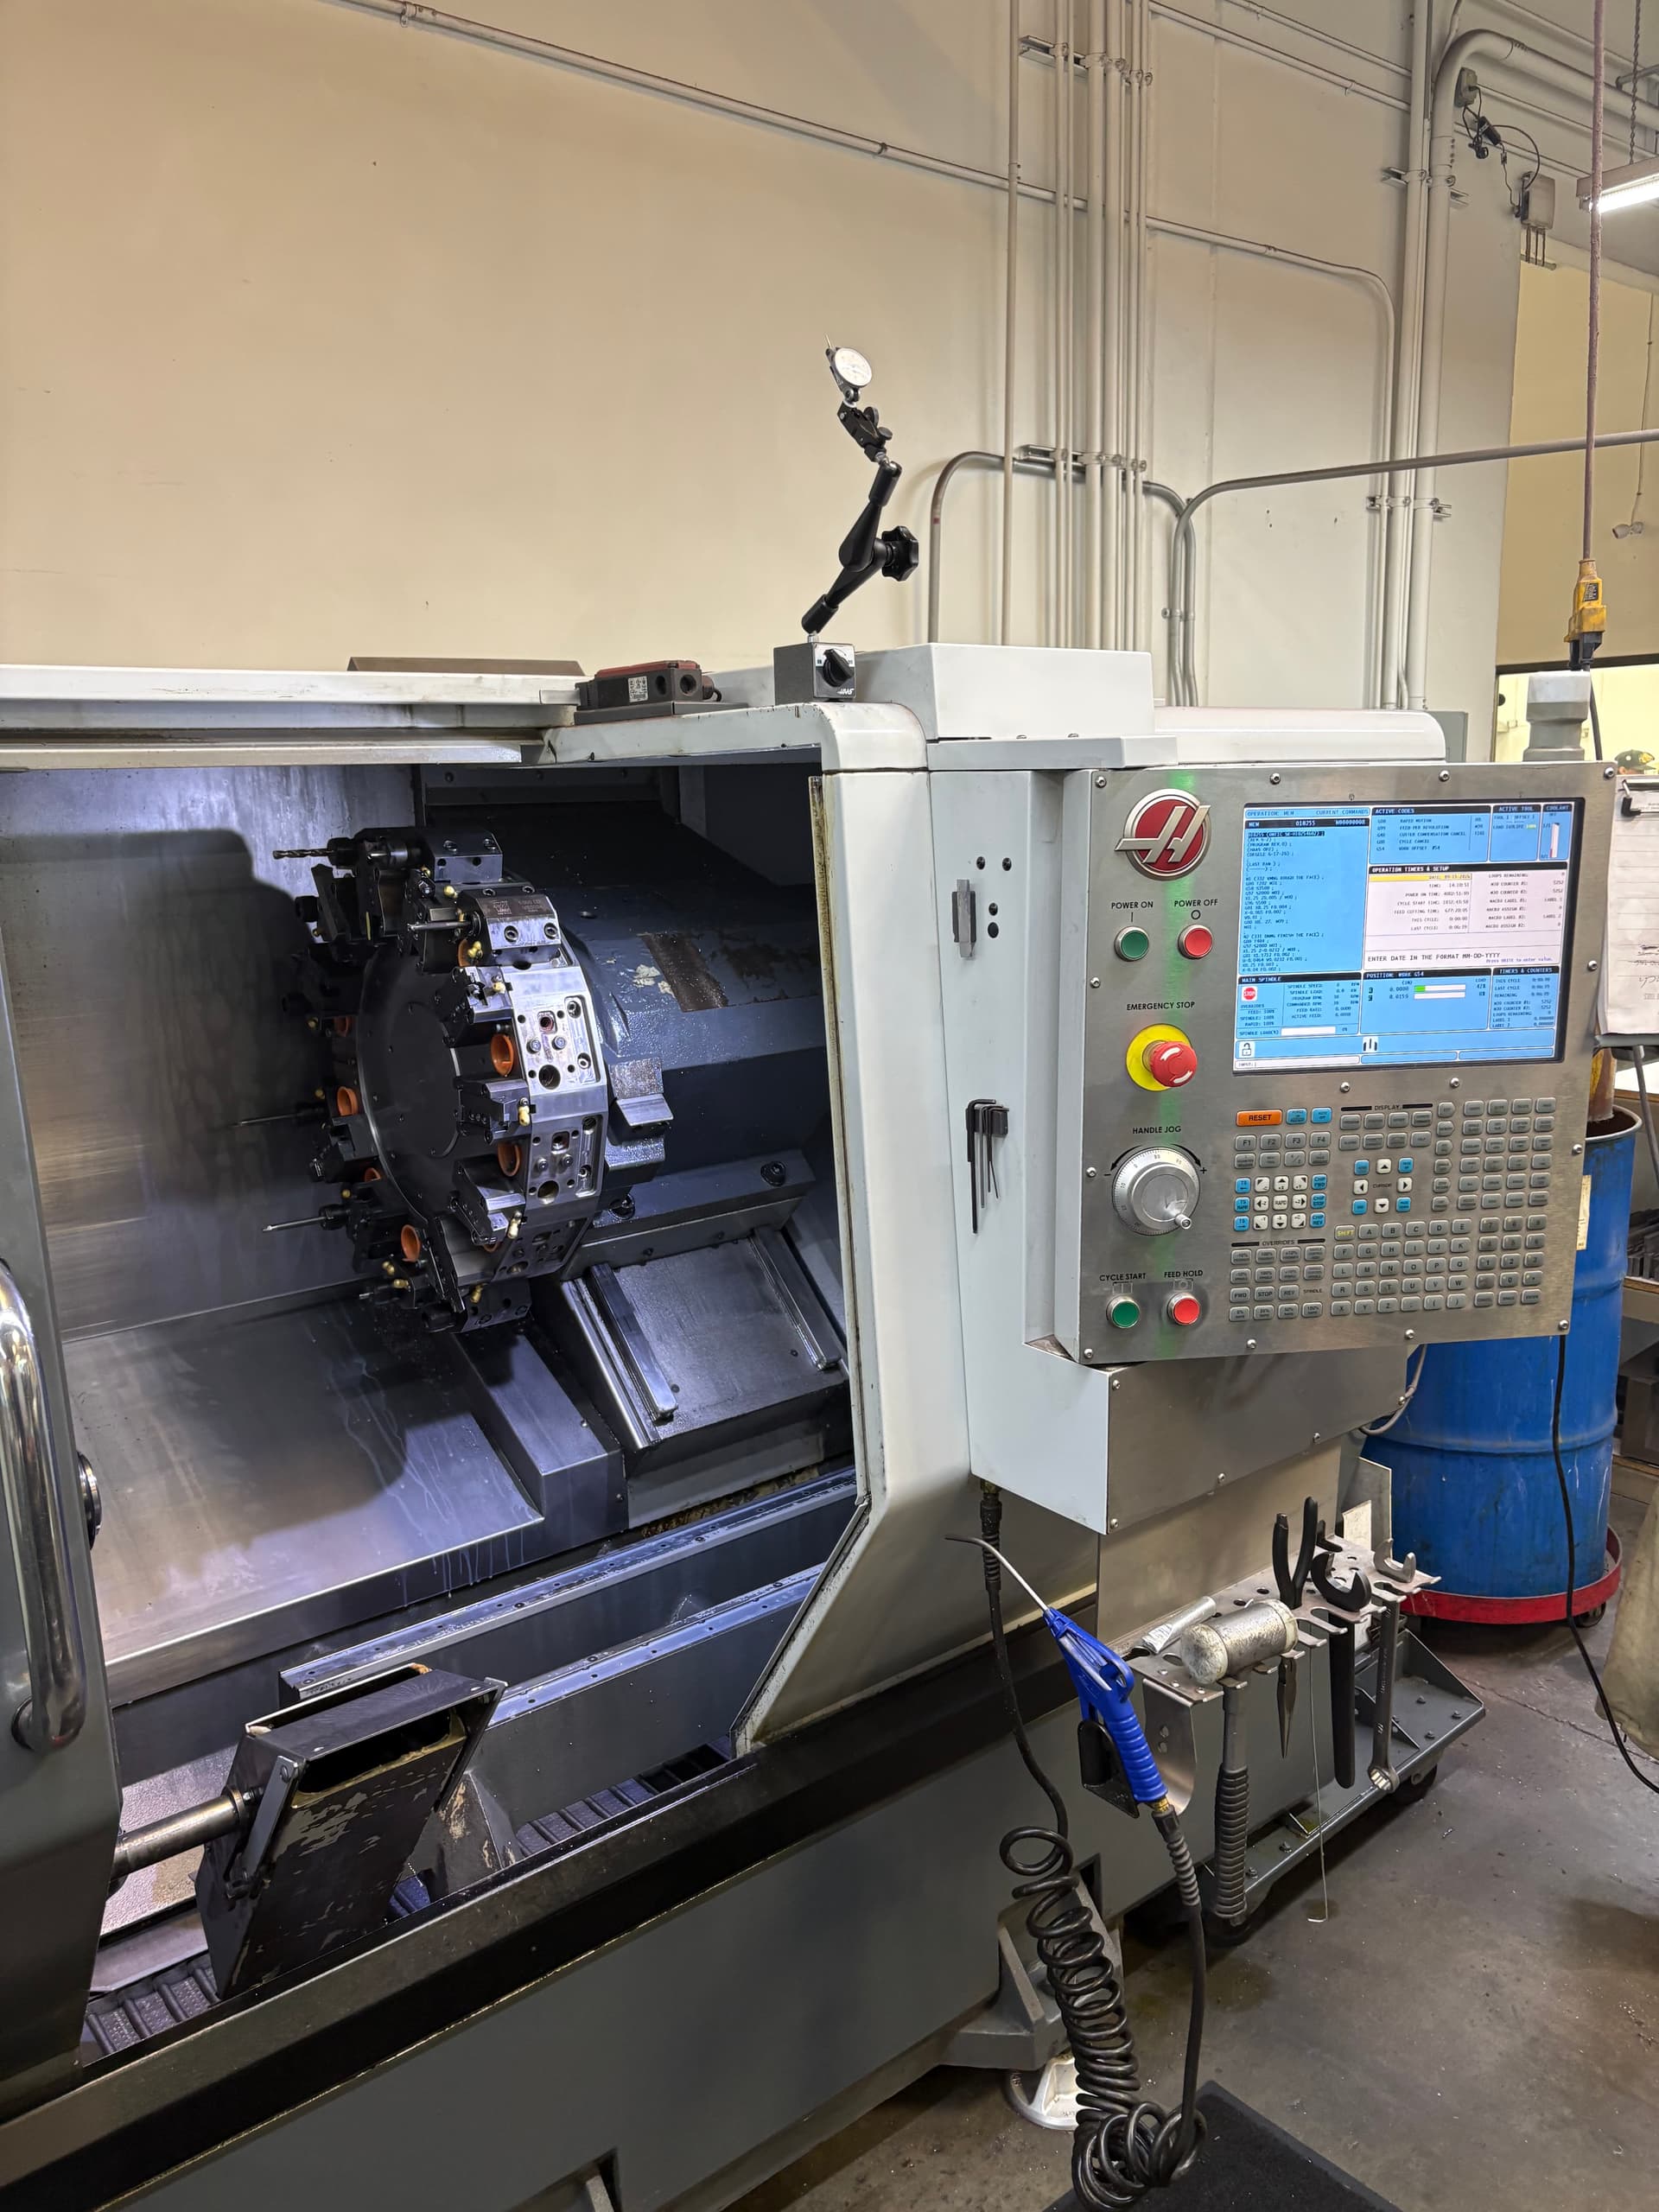
2015 Haas ST-20SS CNC Lathe
USA
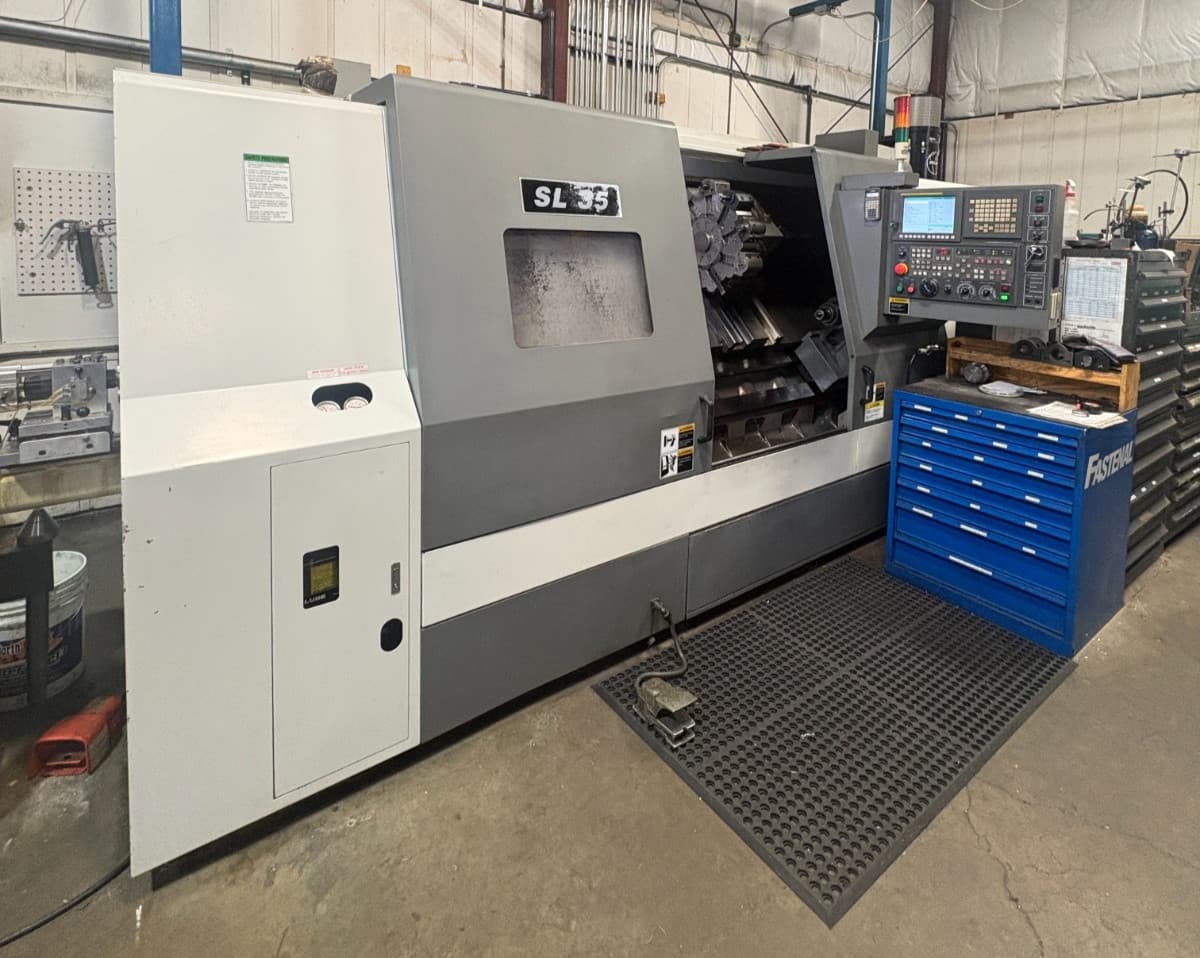
2012 Samsung SL-35A/1500 CNC Turning Center
USA
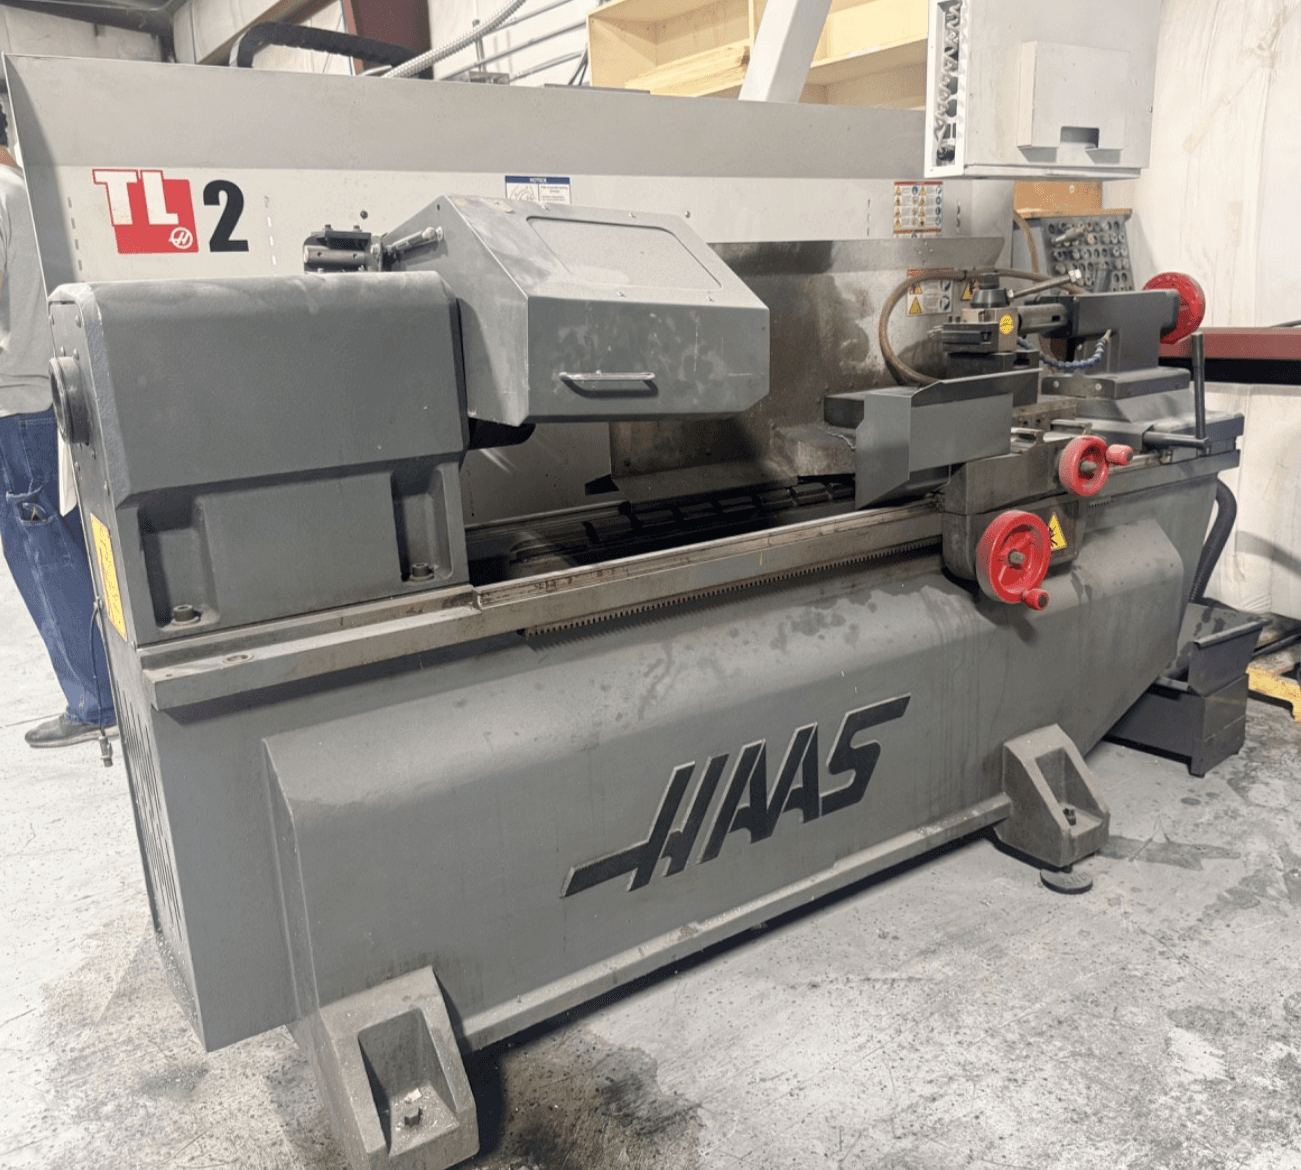
Haas TL-2 CNC Lathe
USA
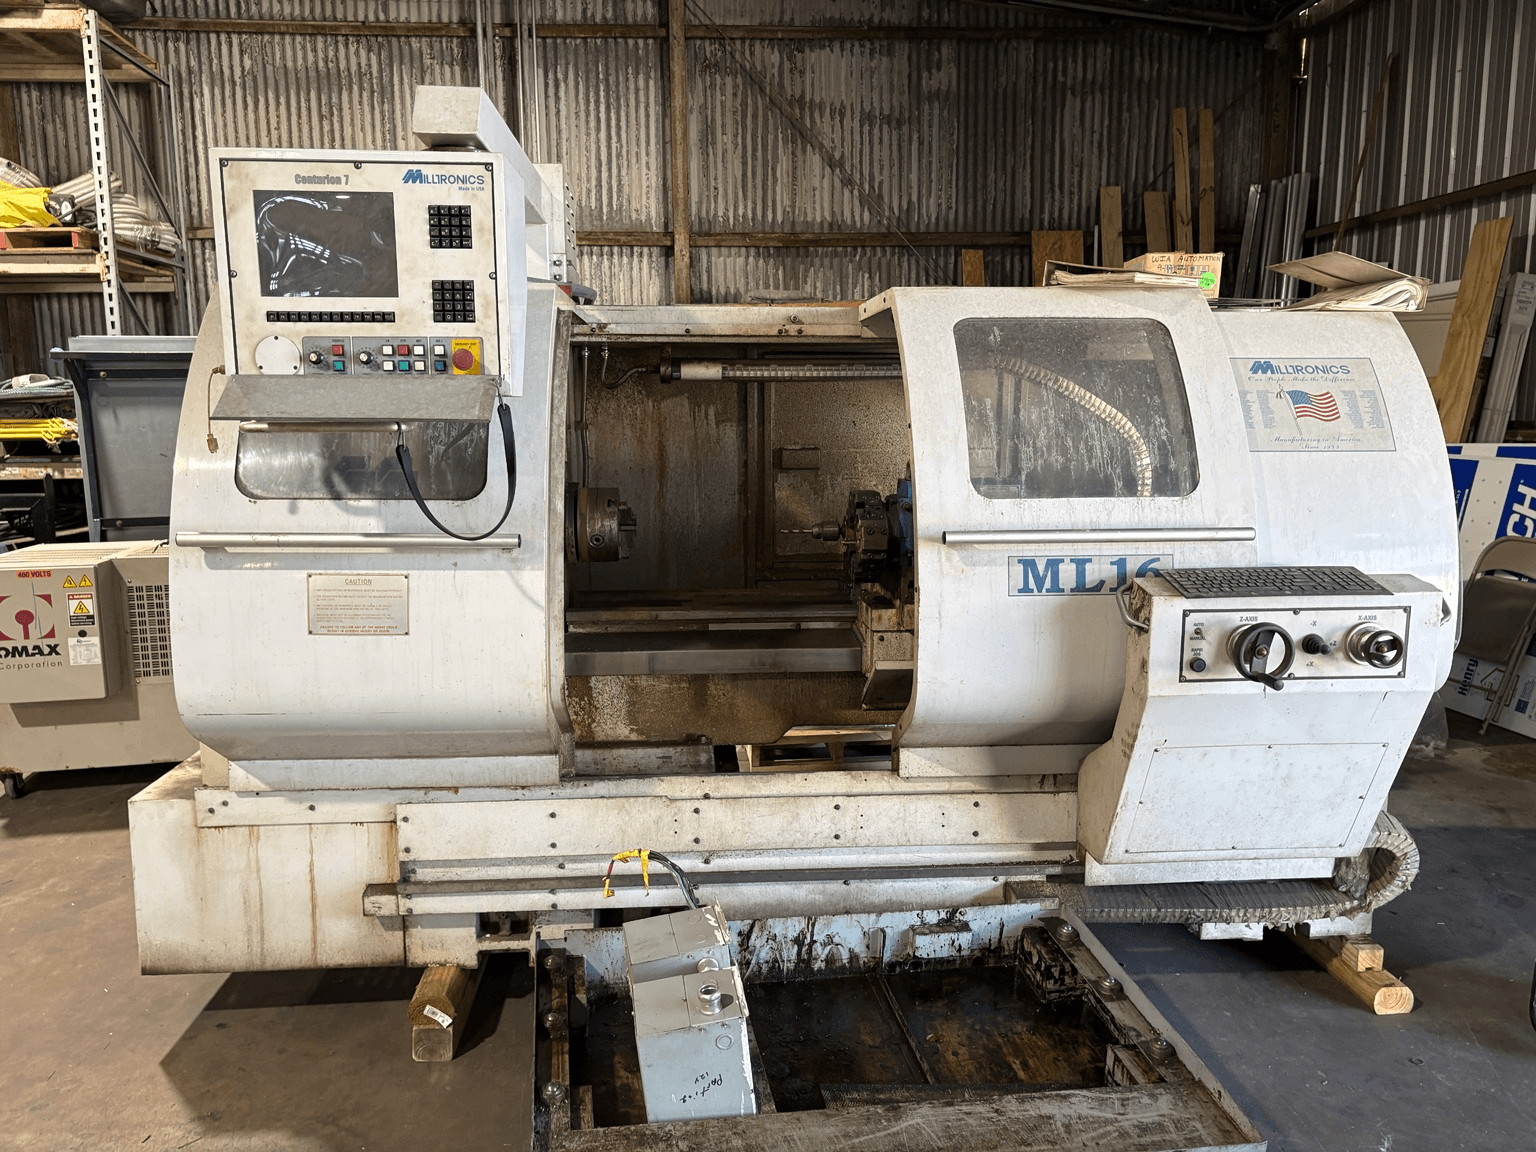
2008 Milltronics ML16 CNC Lathe
USA

2008 Okuma MULTUS B200-W CNC Multitasking Mill-Turn Center w/ LNS Bar Feeder
USA
 Video
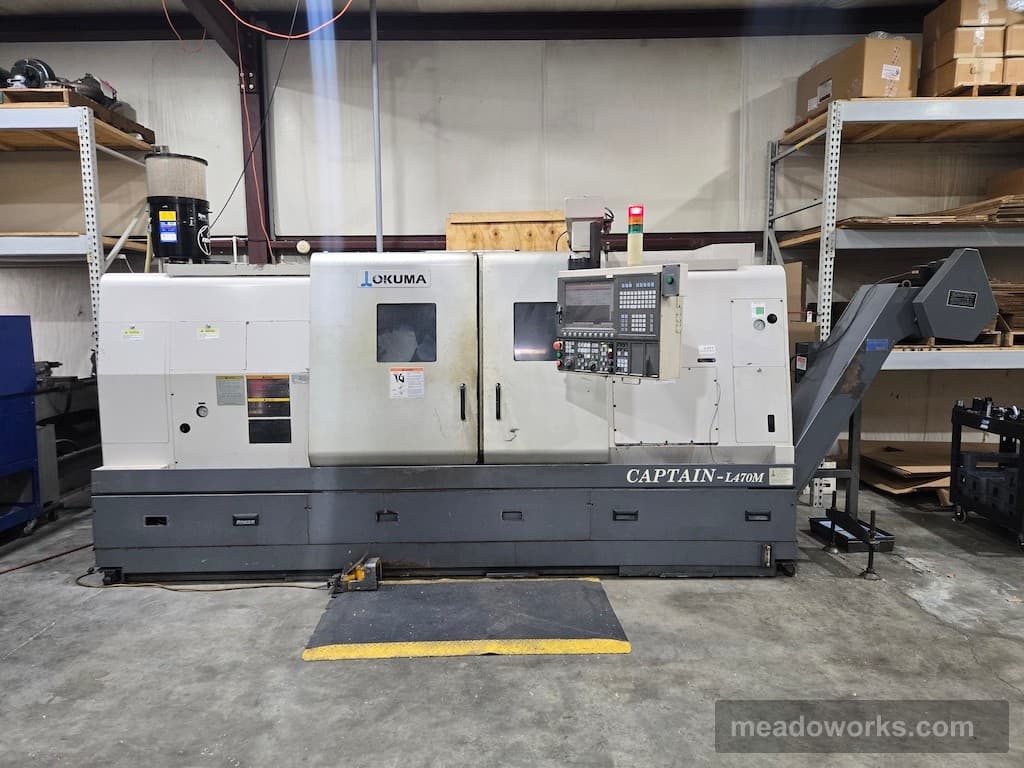
Okuma - Captain L470M
USA
2005 Haas SL-30T CNC Lathe
USA
2004 Mazak Integrex e-650H Mill-Turn Center
USA

FAT/Toolmex TUR 630 MN CNC Lathe
USA
 Video
Mazak Integrex 200SY CNC Multi-Tasking Turn-Mill Center
USA
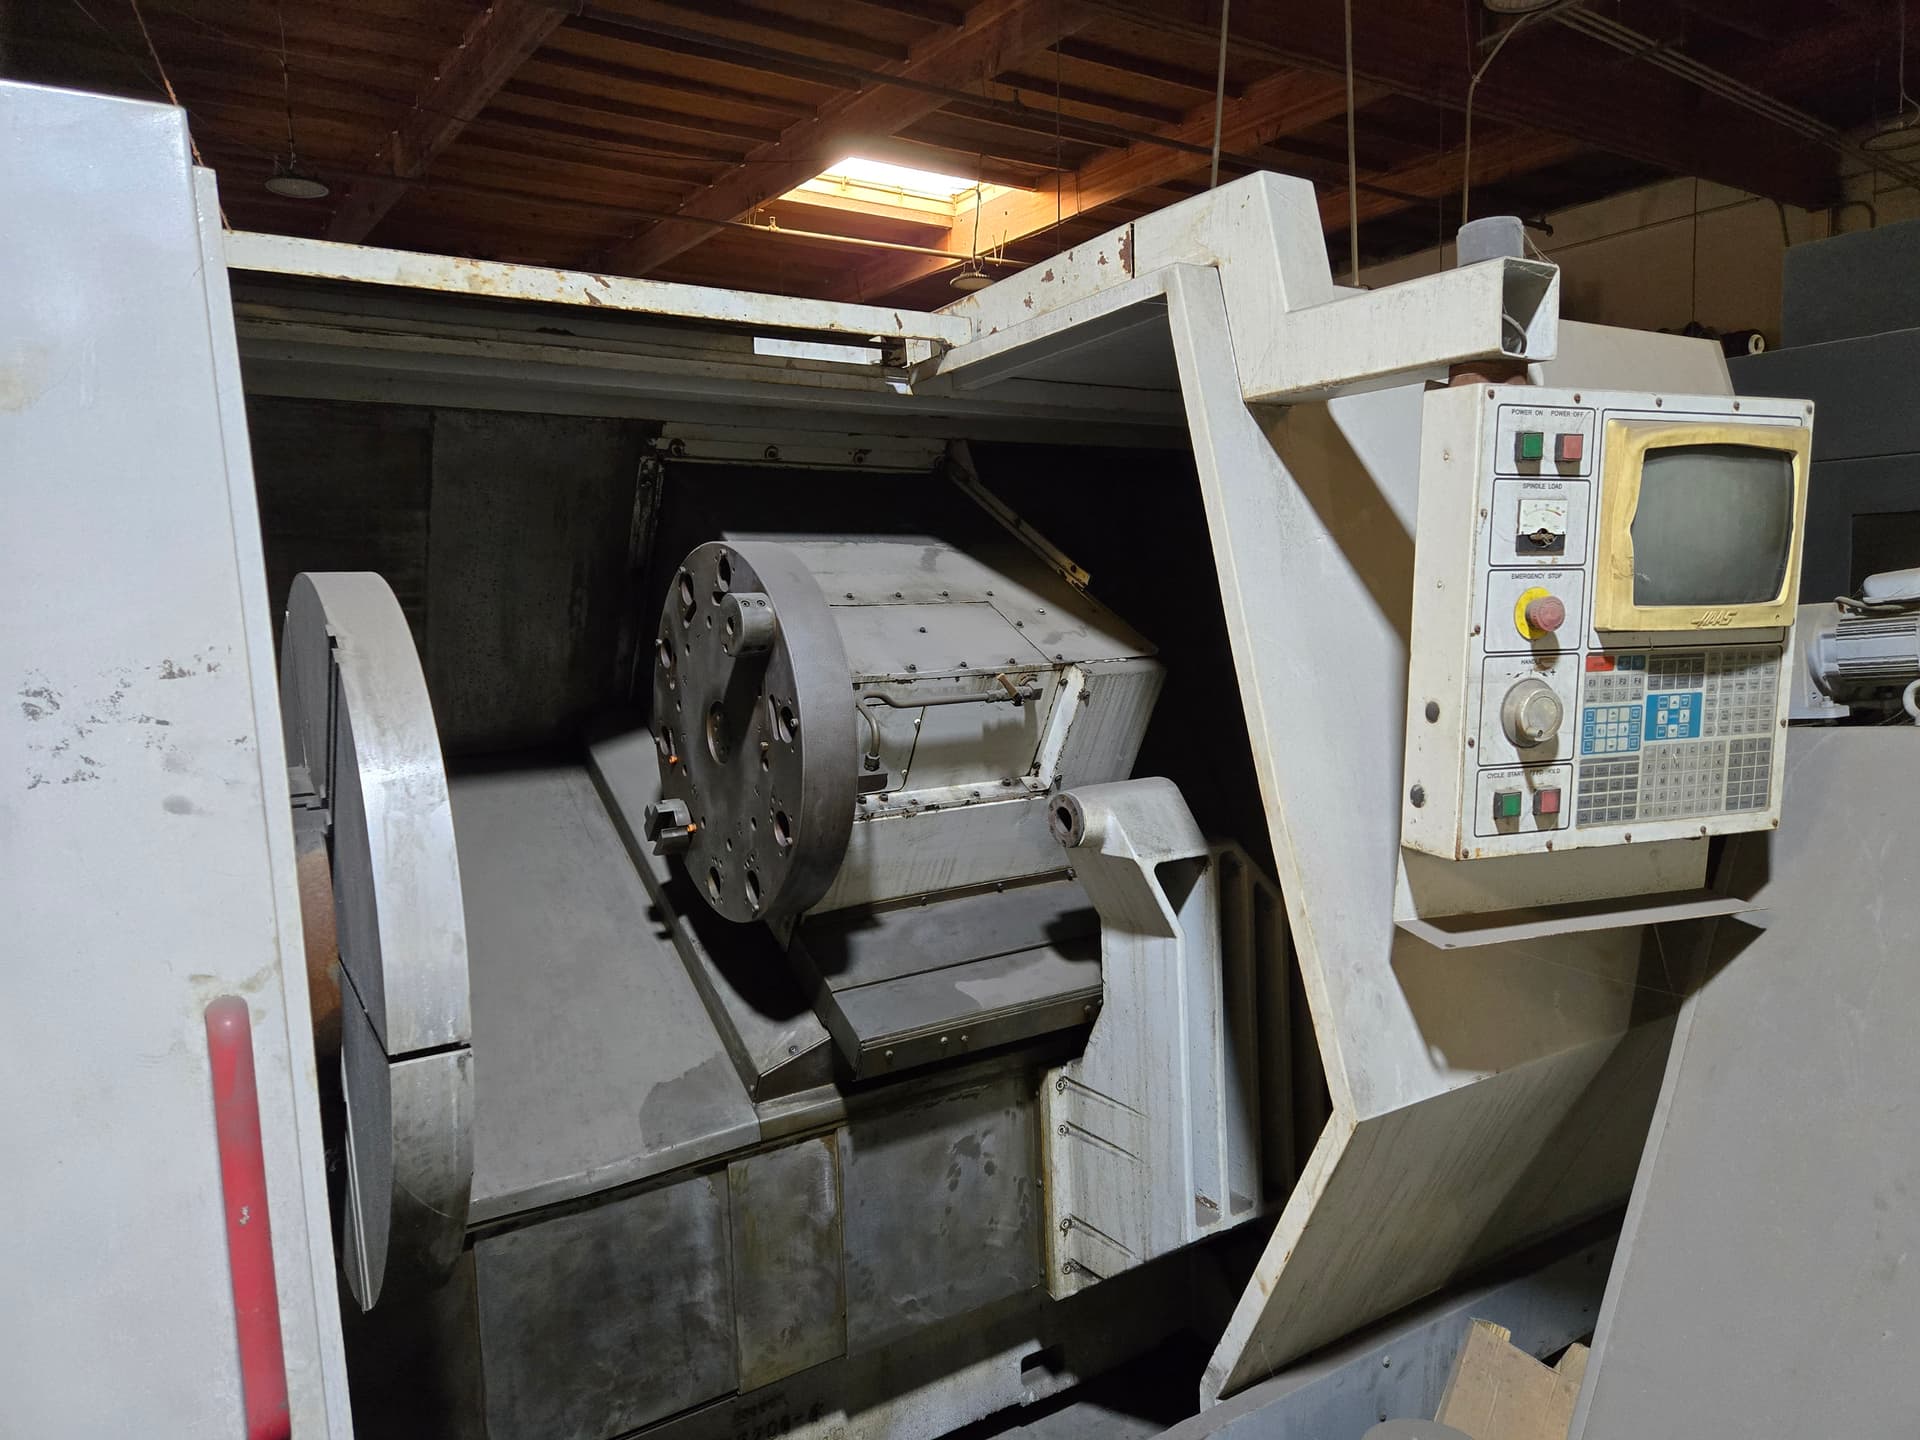
1998 Haas HL-6 CNC Lathe
USA
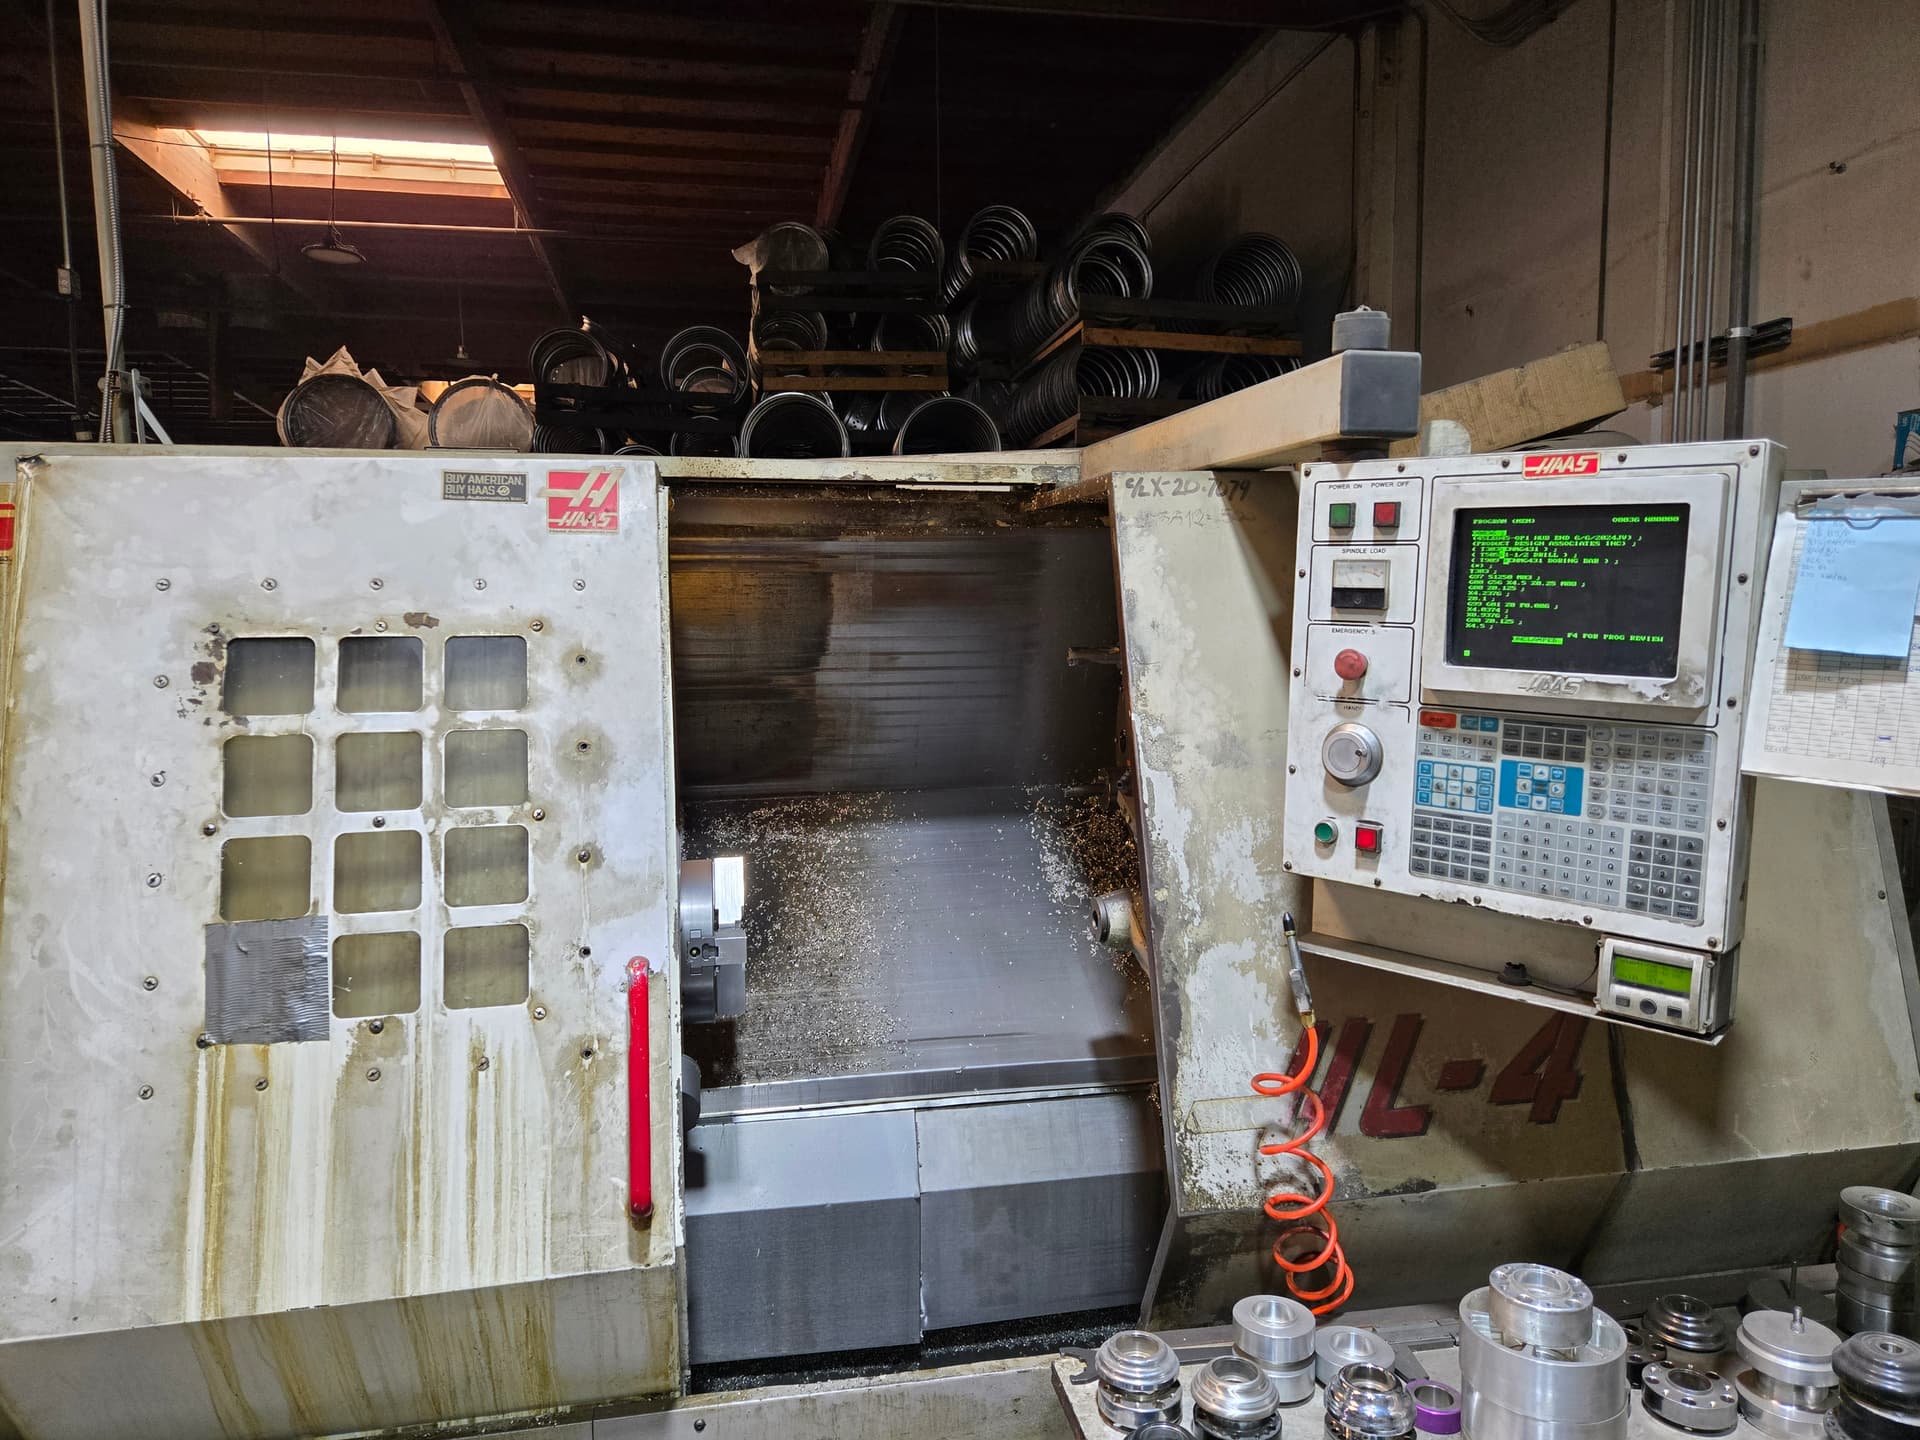
1997 Haas HL-4 CNC Lathe
USA

Mazak Super Quick Turn 28MS CNC Turning Center
USA

Hardinge Cobra 65 CNC Turning Center
USA

Hardinge Cobra 65 CNC Turning Center
USA

Citizen Cincom L25 CNC Swiss-Type Automatic Lathe
USA

Doosan Puma MX2600ST Mill-Turn CNC
USA
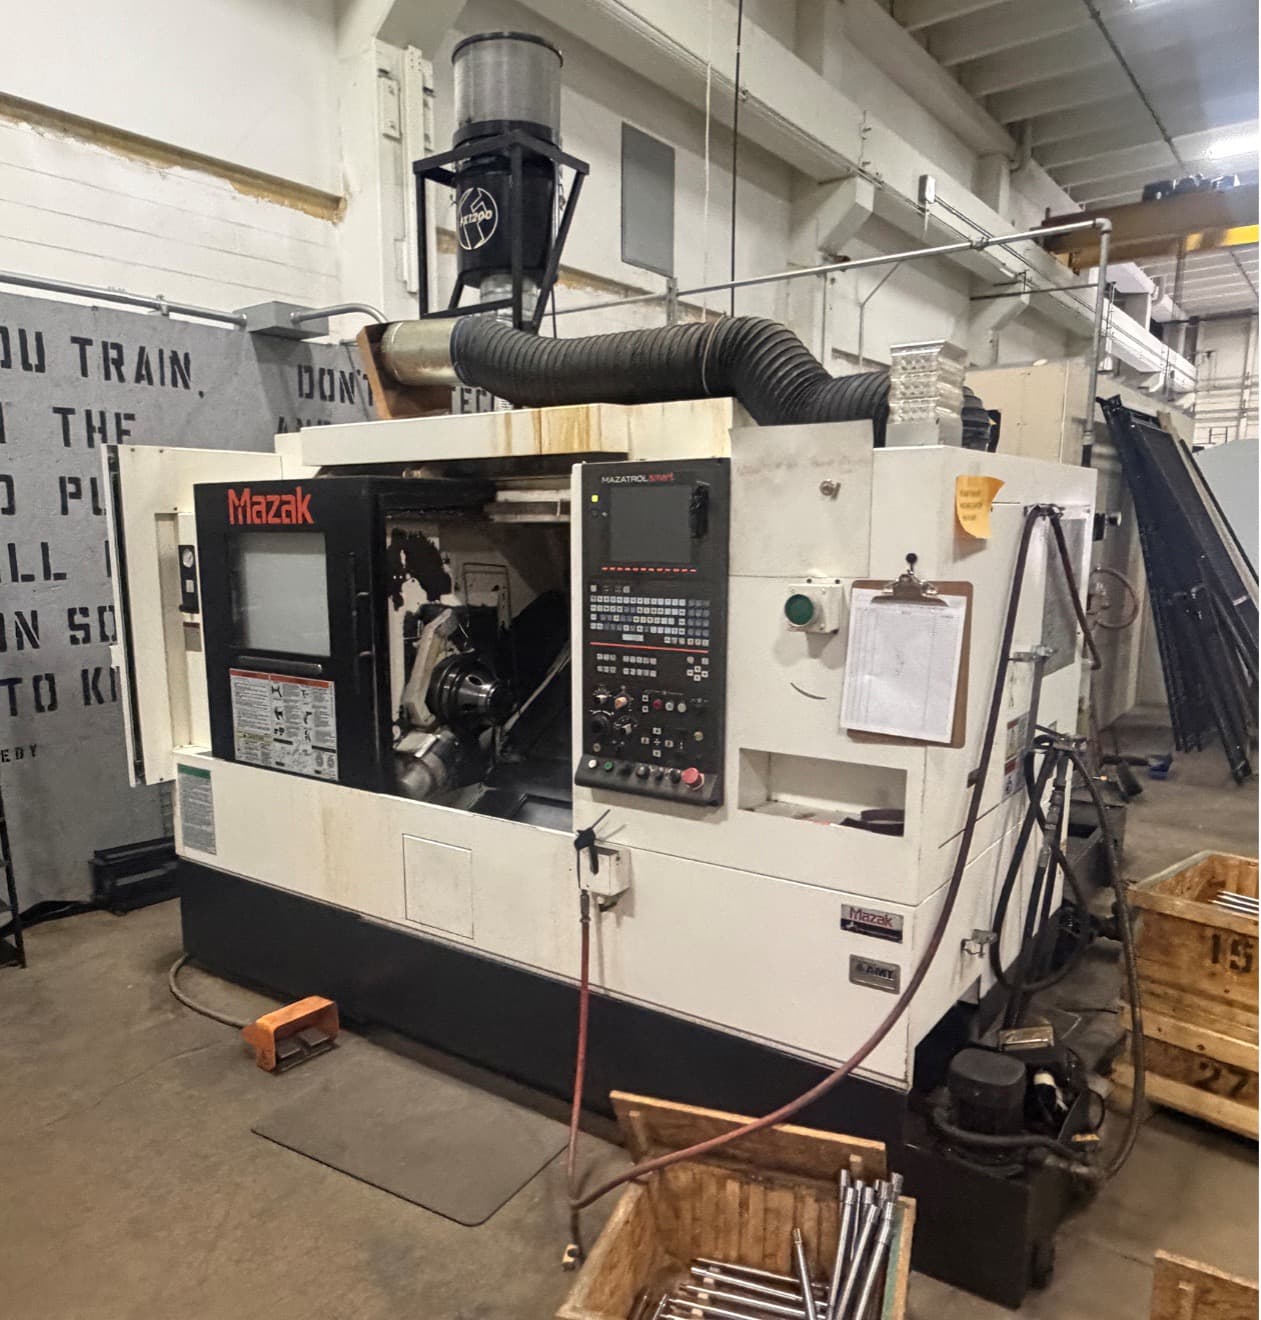
Mazak Quick Turn Smart 250 CNC Turning Center
USA
Looking for Something Specific?
Most of our inventory sells before we can list it online. If you need a specific brand, model, or specification, tell us what you need—we have access to unlisted equipment and machines coming in from plant closures.
Browse Used CNC Lathes by Brand
Browse Used CNC Lathes by Country
Looking to Sell Your CNC Lathes?
Meadoworks is an active cash buyer of used industrial equipment. Get a free valuation from our AMEA-certified appraisers.
About Used CNC Lathes & Turning Centers
CNC lathes and turning centers produce rotational parts including shafts, bushings, fittings, and precision turned components. Modern turning centers add features like live tooling (powered tools for milling/drilling), Y-axis capability, sub-spindles, and bar feeders for complete part production in a single setup. They range from simple 2-axis chucker lathes to complex multi-axis turn-mill centers.
Used CNC lathes are specified by swing (the largest diameter that clears the bed), turning length, bar capacity through the spindle, and the chuck size. A 2-axis lathe turns, faces, bores and threads; a turning center with live tooling (driven tools in the turret) and a Y-axis can also drill, tap and mill off-center features, and a sub-spindle finishes the back of the part so it comes off complete. Slant-bed designs clear chips better and are standard on production turning centers.
When buying used, check spindle bearings and runout, turret indexing and alignment, way and ballscrew wear, the chuck and hydraulic cylinder, and whether a bar feeder or parts catcher is included. Match bar capacity and chuck size to your stock — running bar work saves labor on high-volume parts, while chucker work suits castings and forgings.
This range is broad on purpose. A chucker is a CNC lathe that grips a casting, a forging or a sawed blank and works one end. A turning center is that machine with a turret, and often with live tooling, a Y-axis or a sub-spindle, so a cross hole or the back face does not wait for a second setup. A Swiss lathe is the third layout. The headstock slides and a guide bushing supports small bar, which is how long slender parts stay straight. Swiss machines can sit in this same range. Guide bushing, bar diameter and back-working are compared on the Swiss machine.
Live tooling is a driven station in the turret. It drills, taps and mills a flat while the part stays chucked. It is not a milling spindle that tilts on a B axis. That layout is a mill-turn, on its own machine. A bar feeder, under additional equipment, pushes the next bar when the job is from stock. Swing, turning length, chuck size and bar capacity still come first. Options on a machine that cannot pass the bar will not make the bar fit.
On a used CNC lathe, run the spindle and listen, then index every turret station. Check chuck pressure and the drawtube. Backlash on the carriage and a torn way cover tell you whether the slides still track. If live tooling is why you want the machine, run a driven station under load, not only on the tool machine. Alarm history and a scarred turret are the crash record. Name the control before you count axes.
How to Choose Used CNC Lathes & Turning Centers
How to Size a CNC Lathe
Match swing to the largest diameter you turn, including the chuck jaws, not only the finished print. Then match bar capacity to the stock that must pass the spindle. A chucker with a small bore will not become a bar machine because the turret has more stations.
Turning length has to clear the shaft, the tool and the tailstock or sub-spindle. Chuck size follows the blank, not a habit. Live tooling, a Y-axis and a sub-spindle are the next questions, after the bore and the swing are right. If the part is long, slender and cut from small bar, leave this machine for a Swiss lathe. The guide bushing is the sizing rule there, and a chucker will not imitate it.
Chucker, Turning Center, or Swiss
A chucker holds a discrete blank and turns it. A turning center adds a turret and, when you pay for them, live tooling and a second spindle. A Swiss lathe feeds bar through a guide bushing while the headstock moves. All three can appear in this range because the turning family is wide.
Buy the chucker when the work is castings, forgings or sawed slugs and the second end can be flipped. Buy the turning center when cross holes and a finished back end have to happen in one chucking. Buy the Swiss machine, and read that machine, when the diameter is small and the length would deflect in a chuck. A bar feeder is a separate machine that serves the first two when the job is from bar.
CNC Lathes & Turning Centers Specs to Compare
| Spec | Typical range | Why it matters |
|---|---|---|
| Swing over bed (in) | Often 12–20 in on job-shop chuckers | Swing has to clear the part and the chuck jaws. A short part on a large swing still needs the jaws to clear the bed. |
| Turning length (in) | The shaft, the tool and the tailstock or sub-spindle all have to fit between the chuck and the end of travel. | |
| Bar capacity (in) | Often about 1.5–3 in on a chucker spindle | Bar has to pass the bore. A Swiss machine is sized in millimeters and belongs on the Swiss machine. |
| Chuck size (in) | 6–12 in covers most chucker work | The chuck has to grip the blank you actually load. A larger chuck does not enlarge the bore. |
| Live tooling and Y-axis | Driven turret tools drill and mill off center. A Y-axis reaches features a plain C-axis cannot. | |
| Sub-spindle | The second spindle finishes the back of the part so it does not go to another machine for the cutoff face. |
Swing over bed (in)
Typical range: Often 12–20 in on job-shop chuckers
Swing has to clear the part and the chuck jaws. A short part on a large swing still needs the jaws to clear the bed.
Turning length (in)
The shaft, the tool and the tailstock or sub-spindle all have to fit between the chuck and the end of travel.
Bar capacity (in)
Typical range: Often about 1.5–3 in on a chucker spindle
Bar has to pass the bore. A Swiss machine is sized in millimeters and belongs on the Swiss machine.
Chuck size (in)
Typical range: 6–12 in covers most chucker work
The chuck has to grip the blank you actually load. A larger chuck does not enlarge the bore.
Live tooling and Y-axis
Driven turret tools drill and mill off center. A Y-axis reaches features a plain C-axis cannot.
Sub-spindle
The second spindle finishes the back of the part so it does not go to another machine for the cutoff face.
What to Inspect on Used CNC Lathes & Turning Centers
Run the spindle and listen
Sweep the speed range and ask for spindle hours. A growl is bearings, not a finish problem you can program out.
Index every turret station
Each station should clamp and repeat. One loose station will scrap the tool that lives there.
Check the chuck and drawtube
Jaws, pressure and the hydraulic cylinder should move together. A weak drawtube loses the part in the cut.
Measure carriage backlash
Indicate the slides. Backlash is a ballscrew or a nut, and it appears as a bad shoulder.
Run one live tool
If driven tools are why you are here, cut with one. A station that only spins in the air is not proven.
Read alarms and turret scars
Crash alarms stay in the control. A repaired turret face is the same story in metal.
Match bore, chuck and control
Confirm bar capacity, chuck size and that your crew can program the control. A parts catcher is worth writing down.
Meadoworks Track Record
26
Sold through Meadoworks
23
Listed now
Makes we have handled most
Haas, Tsugami, Mazak, Okuma, Van CNC, Mori Seiki
Common models
Tsugami SS38MH-5AX, Haas ST-10, Hardinge Cobra 65, Van CNC MR38-V7
Related Equipment
- Swiss-Type Lathes
Guide-bushing lathes for long, slender bar
- Mill-Turn Machines
A milling spindle when live tooling is not enough
- Bar Feeders
Magazine and channel feeders for the spindle
Related CNC Lathes & Turning Centers
Mill-Turn & Multitasking Machines
Mill-turn machines (multitasking machining centers) combine full turning and milling capability in a single platform — a turning center with a B-axis milling spindle, or configurations like the Mazak Integrex and DMG Mori NTX series.
Swiss-Type CNC Lathes
Swiss-type CNC lathes (also called sliding headstock or Swiss screw machines) are designed for high-precision, high-volume production of small turned parts.
All CNC Machines
Browse the full used CNC machine inventory — machining centers, lathes, EDM, and more.
Top Brands for Used CNC Lathes & Turning Centers
Haas
US builder of turning centers with its own control.
Tsugami
Japanese builder of Swiss and fixed-headstock turning machines.
Mazak
Japanese builder known for the Mazatrol conversational control.
Van CNC
Okuma
Japanese builder with the OSP control on its turning centers.
Mori Seiki
Japanese lathe builder, later grouped with DMG Mori.
Hardinge
US builder of precision chuckers and toolroom lathes.
Nakamura-Tome
Japanese builder of multi-turret turning centers.
Common Applications
Frequently Asked Questions
How do I match chuck size and bar capacity on a CNC lathe?
Chuck size has to grip the blank. Bar capacity has to pass the stock through the spindle. They are not the same number, and a large chuck on a small bore still will not run bar. Swing has to clear the jaws as well as the part. Turning length has to clear the shaft plus the tool and the tailstock or sub-spindle. Live tooling and a second spindle come after those four.
When is a 2-axis chucker enough instead of a turning center?
When the part is turned, faced, bored and threaded, and any milled feature can wait for another machine. A chucker holds a casting, a forging or a sawed slug and works one end. You flip it for the other end. A turning center earns its turret, live tooling and sub-spindle when a cross hole, a flat or the cutoff face has to be finished in the same chucking. If you never use the driven tools, you paid for a turret you will treat as a gang of turning holders.
What does a sub-spindle finish that the main spindle leaves?
The back of the part. The main spindle turns the outside, the bore and the thread. The sub-spindle takes the part, parts it off and faces or bores the end that was hidden in the chuck. Without it, that face is a second setup, with the error that comes from clamping again. The sub-spindle has to reach, and the part has to fit its chuck or collet. It does not replace a mill when the feature needs a real milling spindle. That is a mill-turn.
How can I tell turret wear from a dull insert on a used lathe?
Index every station and watch the clamp, then indicate a tool tip through a few indexes. A station that does not repeat will move the insert even when the insert is new, and the shoulder will wander. A dull insert on a sound station looks the same on every index and goes away with a fresh edge. Also listen to the spindle and check the drawtube. A part that slips in the jaws looks like a bad tool and is not.
What is live tooling on a CNC lathe?
Live tooling is a driven station in the turret. It drills, taps and mills a flat or a cross hole while the part stays in the chuck. The main spindle still does the turning. The driven station is not a milling spindle on a tilting B axis, and it will not replace a machining center when the feature needs real mill power or a long tool. Ask whether the station has a C axis only, or a Y axis that can move the tool off center. On a used machine, cut with one driven station under load. A holder that only spins in the air has not proved the drive.
What should I check when buying a used CNC lathe?
Run the spindle through its speed range and ask for spindle hours separate from power-on hours. Index every turret station and watch it clamp. Check chuck pressure and the drawtube, then indicate the carriage for backlash. A torn way cover and a scarred turret are the crash record. If the job is from bar, confirm the bore will pass the stock. If you are buying driven tools, cut with one of them. Name the control before you count axes, and confirm the tailstock or sub-spindle still sits on center.
Related Resources
Recently Sold CNC Lathes
View all sold CNC machines →


Looking for Specific CNC Lathes?
Can't find what you need? Contact our team with your requirements. We source equipment from facilities across North America.