Used Machining Centers for Sale
Recently sold
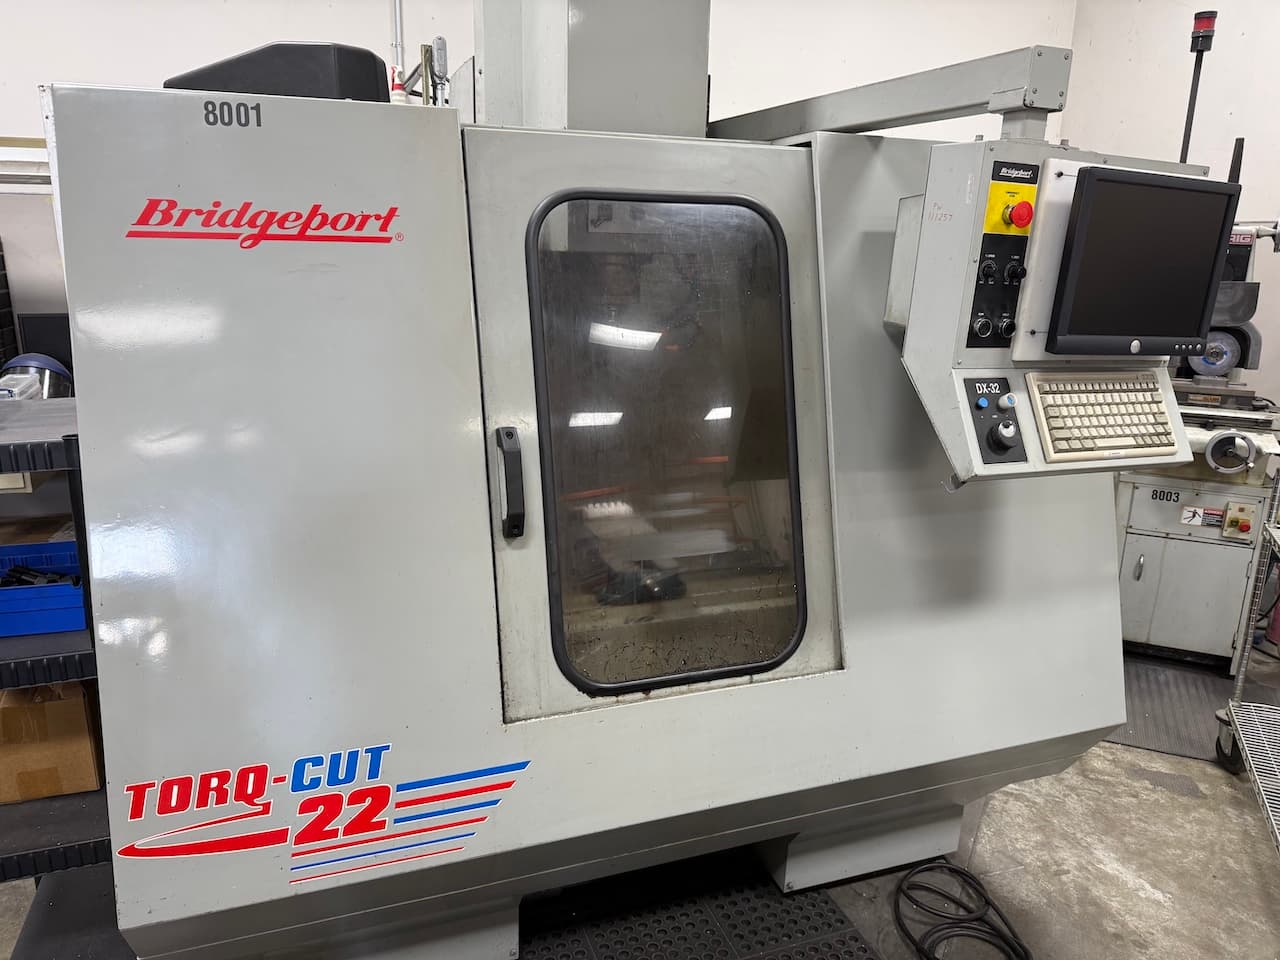 SOLD
Item #6469
Bridgeport CNC Vertical Machining Center
USA
 SOLD
Item #5715
Hurco - VMX42
USA
 SOLD
Item #5825
Haas VF-2DTR CNC Vertical Machining Center
Mexico
 SOLD
Item #5828
Haas VF-2DTRHE CNC Vertical Machining Center
Mexico
 SOLD
Item #5826
Haas VF-2DTR CNC Vertical Machining Center
Mexico
 SOLD
Item #5823
Haas VF-2TR CNC Vertical Machining Center
Mexico
 SOLD
Item #5824
Haas VF-2DTR CNC Vertical Machining Center
Mexico
 SOLD
Item #5827
Haas VF-2DTR CNC Vertical Machining Center
Mexico
 SOLD
Item #5822
Haas VF-2TR CNC Vertical Machining Center
Mexico
 SOLD
Item #5858
2022 Haas VF-2SS
USA
 SOLD
Item #6112
Milltronics Partner 7 Series H VMC
USA
 SOLD
Item #6111
Hurco VMX24
USA
 SOLD
Item #6108
2006 Fadal VMC 6030
USA
 SOLD
Item #6110
2006 Hurco VMX42
USA
 SOLD
Item #6109
2005 Fadal VMC 6030 HT
USA
 SOLD
Item #6234
2004 Brother TC-S2B-0 CNC Tapping Center
USA
 SOLD
Item #6227
1998 Mori Seiki SV-5000 CNC Vertical Machining Center
USA
 SOLD
Item #6229
2006 Leadwell MV-40 CNC Vertical Machining Center
USA
 SOLD
Item #6232
2005 Mori Seiki Duracenter 5 CNC Vertical Machining Center
USA
 SOLD
Item #6226
1997 Fanuc Robodrill a-T14iA CNC Drill & Tap Machine
USA
 SOLD
Item #6231
2006 Mori Seiki Duracenter 5 CNC Vertical Machining Center
USA
 SOLD
Item #6225
1997 Fanuc Robodrill a-T14iA CNC Drill & Tap Machine
USA
 SOLD
Item #6235
2003 Brother TC-S2B CNC Tapping Center
USA
 SOLD
Item #6222
2000 Fadal VMC 3016L CNC Vertical Machining Center
USA
Machining Centers by the numbers
From our own catalog: machines listed now and machines we have sold. Updated every few minutes.
Our track record
55 machines sold · 14 makes · model years 1986–2022 · 21 sold at our own auctions
By brand
| Brand | In stock now | Sold by Meadoworks | Model years |
|---|---|---|---|
| Haas | 8 | 11 | 1995–2023 |
| Doosan | 4 | 1 | 2008–2019 |
| Milltronics | 3 | 1 | 2006–2015 |
| Matsuura | 3 | 0 | 2001–2018 |
| Hurco | 2 | 3 | 2006–2011 |
| DMG Mori | 2 | 0 | 2011–2018 |
| Mori Seiki | 1 | 7 | 1998–2011 |
| Bridgeport | 1 | 1 | — |
| Daewoo | 1 | 0 | 2001 |
| Datron | 1 | 0 | — |
Looking for Something Specific?
Most of our inventory sells before we can list it online. If you need a specific brand, model, or specification, tell us what you need—we have access to unlisted equipment and machines coming in from plant closures.
Looking to Sell?
Meadoworks is an active cash buyer of used industrial equipment. Get a free valuation from our AMEA-certified appraisers.
About Used Machining Centers
A machining center is a CNC mill with an automatic tool changer. The control calls the next tool, the spindle cuts, and the operator is not standing there with a wrench between operations. That single feature is what separates the category from a knee mill. Everything else, vertical or horizontal spindle, three axes or five, is a choice about the parts you run, not a different kind of machine.
Four configurations cover almost every buyer. A vertical machine points the spindle down at a table. It is the default for plates, housings, mold bases and the mixed work a job shop sees in a week. A horizontal machine points the spindle sideways, usually with a rotary table, so chips fall out of a bore and a pallet can be loaded while the other pallet is cutting. A 5-axis machining center adds two rotary axes, either under the part or in the head, for contours and for faces you would otherwise re-fixture. A drill-tap center is a small, fast vertical machine built for holes, taps and light milling on parts that do not need a 40-inch table. Pick the configuration from the part and the batch size. Then pick the brand.
The machining center is the middle of a metalworking cell, not the whole cell. A knee mill or an engine lathe still earns its floor space for one-off work and for second ops that are awkward in a vise. A CNC lathe owns round parts. A horizontal with a tombstone owns a family of prismatic parts that repeat. Inspection, whether a height gage or a coordinate measuring machine, sits after the cut. Buying a second vertical machine because the first one is full is a different decision from buying a horizontal because the parts have four sides and the chips are packing the pockets.
What holds value on a used machining center is the iron and a control your people can still program and repair. Travels, taper and tool-changer size are the facts that decide fit. Spindle hours and a crash history decide the repair bill. A 4th-axis rotary on a vertical machine is often the cheaper path to multi-side work. A full 5-axis machine is the path when the rotary cannot reach the surface. Budget time for rigging, a level, and an electrical drop. The control options, probing and through-spindle coolant, are worth more than fresh paint.
Meadoworks takes machining centers off shops that are consolidating, from plant closures, and from auctions where a cell is sold together. Listings carry travels, taper and the control name, and a buyer can inspect the machine under power when the site allows it. We coordinate rigging and trucking with crews who move machine tools, so the spindle and the way covers are not an afterthought on the bill of lading.
How to Choose a Used Machining Center
How to Choose a Vertical, Horizontal or 5-Axis Machining Center
Start with the part, then the batch. One or two setups, a vise, and a mix of jobs point to a vertical machine. Four sides, a repeating family, and chips that pack a pocket point to a horizontal with a pallet and a tombstone. A surface the tool cannot reach without tilting the part, or a stack of setups you want to delete, points to 5-axis. A part that is mostly drilled and tapped, in high volume and small size, points to a drill-tap center rather than a full vertical machine you will never use the travels on.
Do not buy the largest table you can afford and call it flexibility. Unused travel is floor space and a longer way system. Match X, Y and Z to the part plus the fixture, with room for the tool. Then standardize. A shop that already owns CAT40 holders should not add a BT50 machine unless the cut requires it.
Taper, Control and Tooling Before the Brand
The spindle taper decides which holders you already own. CAT40 and BT40 cover most vertical work. CAT50 is for heavy roughing. A drill-tap machine may be BT30. Mixing tapers means a second drawer of holders. The control decides who can run the machine on Monday. Haas, Fanuc, Mazatrol and Hurco WinMax are common on the used market, and a control your crew has never seen is a training project, not a capacity project.
Tool-changer capacity should cover the part family without a manual swap in the middle of the cycle. Twenty to thirty tools is a normal vertical magazine. Horizontals often carry more because the tombstone presents more operations. Probing and through-spindle coolant are options you can add later on some machines and not on others. Ask before you treat them as stickers.
By Class: Used Machining Center Price Ranges
Drill-tap centers and small 40-taper verticals, under 30 in of X: about $15,000–$60,000.
Mid-size verticals, 30–50 in of X: about $25,000–$90,000.
Horizontals with pallet changers: about $60,000–$300,000.
5-axis trunnion and swivel-head machines: about $80,000–$400,000.
What moves the price: age and control generation, spindle hours and condition, through-spindle coolant, a chip conveyor, probing, the tool changer count and the tooling that comes along. These are typical used-market ranges, not a quote on any one machine. Call 800-323-0307 for a current price.
Machining Center Specs to Compare
| Spec | Typical range | Why it matters |
|---|---|---|
| Axis travels (in) | 20–60 in X on most verticals | Travels have to clear the part and the fixture, not just the print of the finished piece. |
| Spindle taper | CAT40, BT40, or CAT50 | The taper has to match the holders you already own or you are buying a second set. |
| Spindle speed (rpm) | 8,000–12,000 on general work | Higher speed helps aluminum and small tools. Steel roughing cares more about low-end torque. |
| Tool capacity | 20–40 tools on a vertical | The magazine has to hold the part family or someone swaps tools by hand mid-cycle. |
| Table load (lb) | A heavy fixture plus the part can exceed a small machine even when the travels look fine. | |
| Control | Fanuc, Haas, Mazatrol and WinMax are programmable by different crews. Match the people you have. |
Axis travels (in)
Typical range: 20–60 in X on most verticals
Travels have to clear the part and the fixture, not just the print of the finished piece.
Spindle taper
Typical range: CAT40, BT40, or CAT50
The taper has to match the holders you already own or you are buying a second set.
Spindle speed (rpm)
Typical range: 8,000–12,000 on general work
Higher speed helps aluminum and small tools. Steel roughing cares more about low-end torque.
Tool capacity
Typical range: 20–40 tools on a vertical
The magazine has to hold the part family or someone swaps tools by hand mid-cycle.
Table load (lb)
A heavy fixture plus the part can exceed a small machine even when the travels look fine.
Control
Fanuc, Haas, Mazatrol and WinMax are programmable by different crews. Match the people you have.
What to Inspect on a Used Machining Center
Run the spindle through its range
Listen at low and high rpm. A roar or a heat climb is bearings. Ask for spindle hours separately from power-on hours.
Check backlash on each axis
A dial indicator or the control's diagnostic screen will show a worn ballscrew. One bad axis is a rebuild, not a lubricant issue.
Cycle every tool pocket
Run the changer twice through the magazine. A single pocket that alarms is an arm or a carousel, and it will stop production.
Read the alarm history
Servo overloads and crash alarms stay in the control. Fresh paint over a bent sheet-metal head is a story. Ask for it.
Confirm taper and pull studs
CAT and BT holders do not interchange. The drawbar has to grip the pull stud or tools slip under load.
Look at way covers and wipers
Torn covers let chips grind the ways. The cover is cheap. The way under it is not.
Identify the control generation
A control with no parts and no one who can program it is a conversion project. Price that before you price the iron.
Note the options that matter
Fourth axis, probing, through-spindle coolant and a chip conveyor change what the machine can run on the first day.
Related Equipment
- Used Vertical Machining Centers (VMC)
The default spindle-down machine for mixed work
- Used Horizontal Machining Centers (HMC)
Pallets and chip evacuation for repeating parts
- Used 5-Axis Machining Centers
When a rotary on a 3-axis machine cannot reach
- Used Drill & Tap Centers
Fast hole work that does not need a large table
Machining Centers Brands We've Sold
Haas
US builder of vertical machining centers with its own control.
Makino
Japanese builder known for rigid, high-accuracy machining centers.
Mori Seiki
Japanese machining centers, later part of DMG Mori.
Brother
Japanese builder of fast drill-tap and compact machining centers.
Doosan
Korean builder of machining centers, now sold as DN Solutions.
Hurco
Indianapolis builder known for the conversational WinMax control.
Fadal
American vertical machining centers with a large installed base.
Milltronics
US builder of conversational machining centers for job shops.
Common Applications
Frequently Asked Questions
What is a machining center, as opposed to a CNC mill?
A machining center is a CNC mill with an automatic tool changer and a control that swaps tools in the program. A knee mill, and many lighter CNC mills, still expect a person to change the tool. Once the changer is there, the real choices are spindle direction, how many axes move, and whether a pallet lets you load the next part while the spindle is cutting. Those choices are vertical, horizontal, 5-axis and drill-tap. They are configurations of a machining center, not separate industries.
Should a job shop buy a vertical or a horizontal machining center first?
Buy a vertical machine first if the work is mixed, the batches are short, and the parts sit in a vise. It is easier to set, it uses less floor, and the holders are the ones most shops already own. Buy a horizontal first only if you already know the parts have several faces, the volume will keep a pallet busy, and chips are a problem in the pockets. A horizontal that runs one prototype a day is an expensive vise. A vertical that tries to be a production cell will spend its life in setup.
When is a 5-axis machining center worth it instead of a rotary on a vertical?
A rotary table on a vertical machine indexes a part so you can mill several sides in one clamping. That is enough for a lot of brackets and valve bodies. A 5-axis machine is worth it when the tool has to keep moving while the part tilts, or when the tilt has to be a programmed angle rather than a manual index. Contoured surfaces, undercuts and parts you are re-fixturing four times belong there. If a rotary and a good fixture would delete the extra setups, buy the rotary.
What should I check on a used machining center?
Run the spindle across its speed range and ask for spindle hours. Check backlash on each axis and cycle the tool changer through every pocket. Read the alarm history for crashes and servo faults. Confirm the taper matches your holders and that the drawbar still grips a pull stud. Look at the way covers. Then name the control and decide whether your crew can program it. Options worth writing down are a fourth axis, probing, through-spindle coolant and a chip conveyor. Paint does not tell you any of that.
What does a CNC machining center for sale usually mean?
It means a CNC mill with a tool changer, which is the phrase buyers type. The description still has to say whether the spindle is vertical or horizontal, what the travels are, what the taper is, and which control is on the door. A drill-tap center and a 50-taper vertical machine can both wear that phrase. Read the configuration before you compare two machines. Vertical, horizontal, 5-axis and drill-tap layouts are different tools for different parts, and the phrase alone does not sort them.
Do I need through-spindle coolant on a machining center?
You need it for deep holes, for taps that pack chips, and for production work where the operator cannot stand there with a nozzle. A machine without it can still mill faces, pockets and most job-shop plates if the flood coolant reaches the cut. Adding it later is possible on some builders and a rebuild on others. If your parts are mostly drilled, treat it as a requirement. If your parts are mostly milled open features, treat it as a useful option and do not walk away from a sound spindle over a missing pump.
Buying Guides
VMC vs HMC: Which CNC Machining Center Do You Need?
When a vertical machine is enough and when a horizontal earns the floor space.
Read GuideCNC Machine Inspection Checklist
Spindle, ballscrews, control and tool changer, in the order that matters.
Read Guide5-Axis CNC Machine Buying Guide
Positional 3+2 versus simultaneous five-axis, and the two rotary layouts.
Read Guide