Used Knee Mills for Sale
4 results
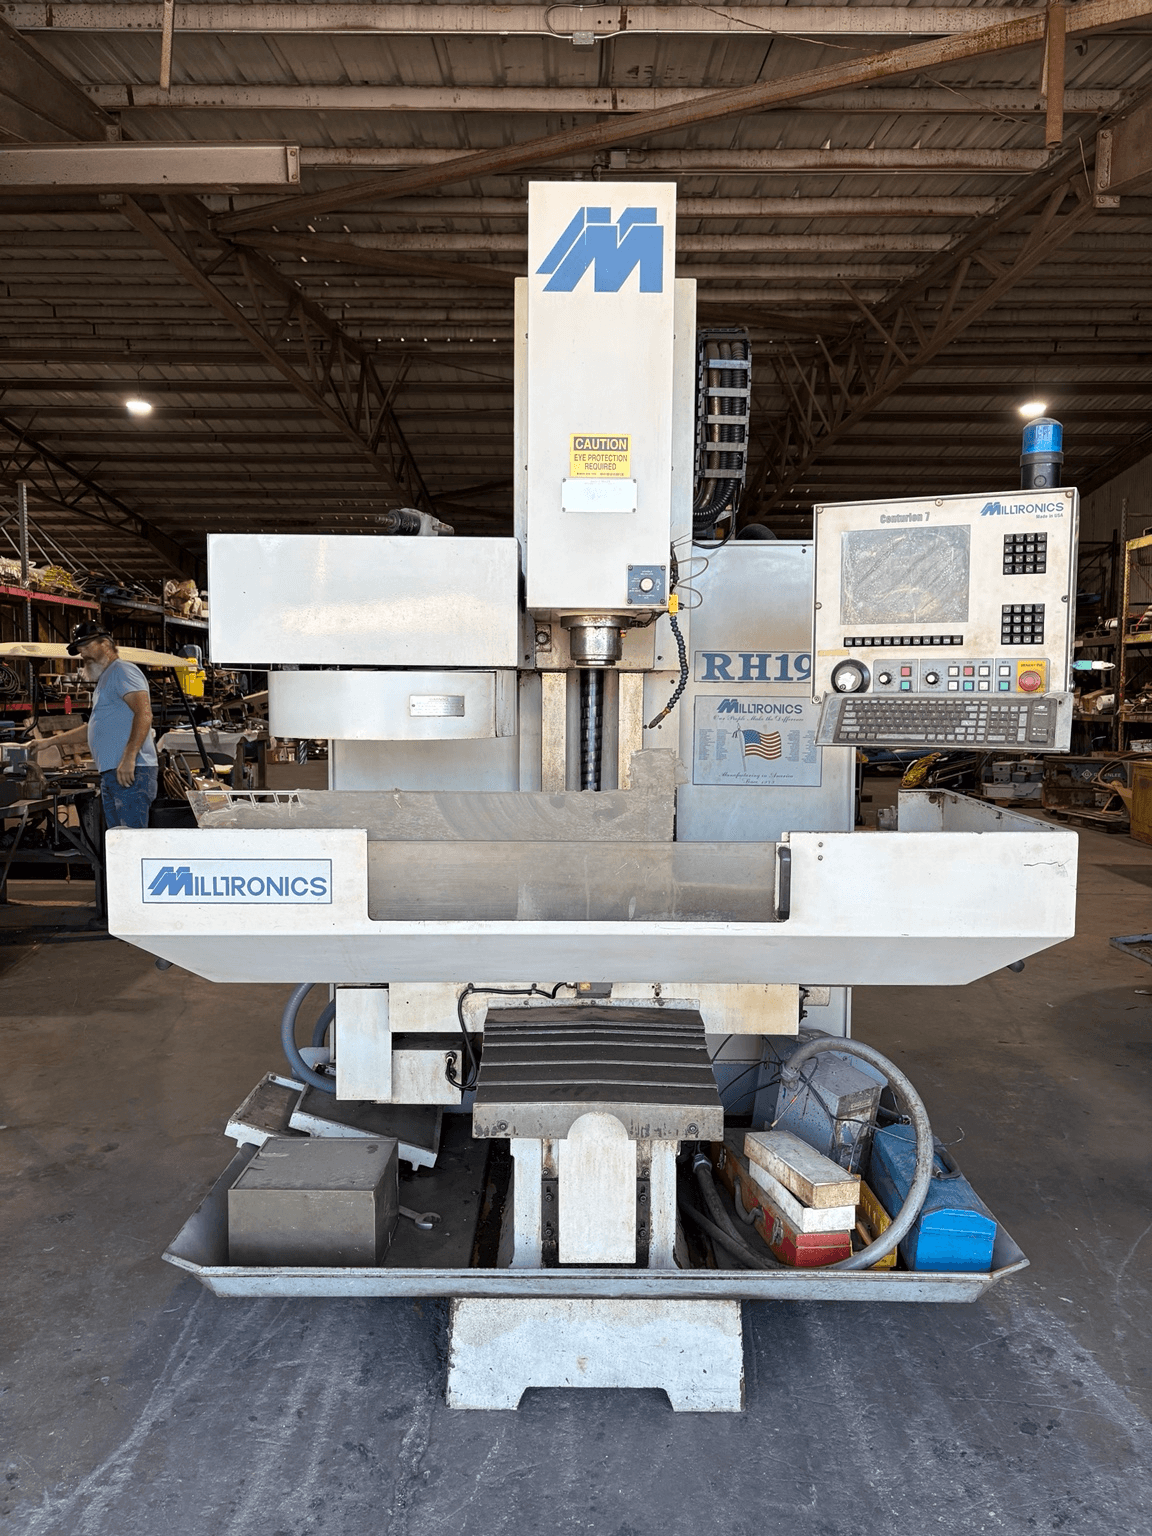
2012 Milltronics RH19 Bed Mill
USA
Lot 14
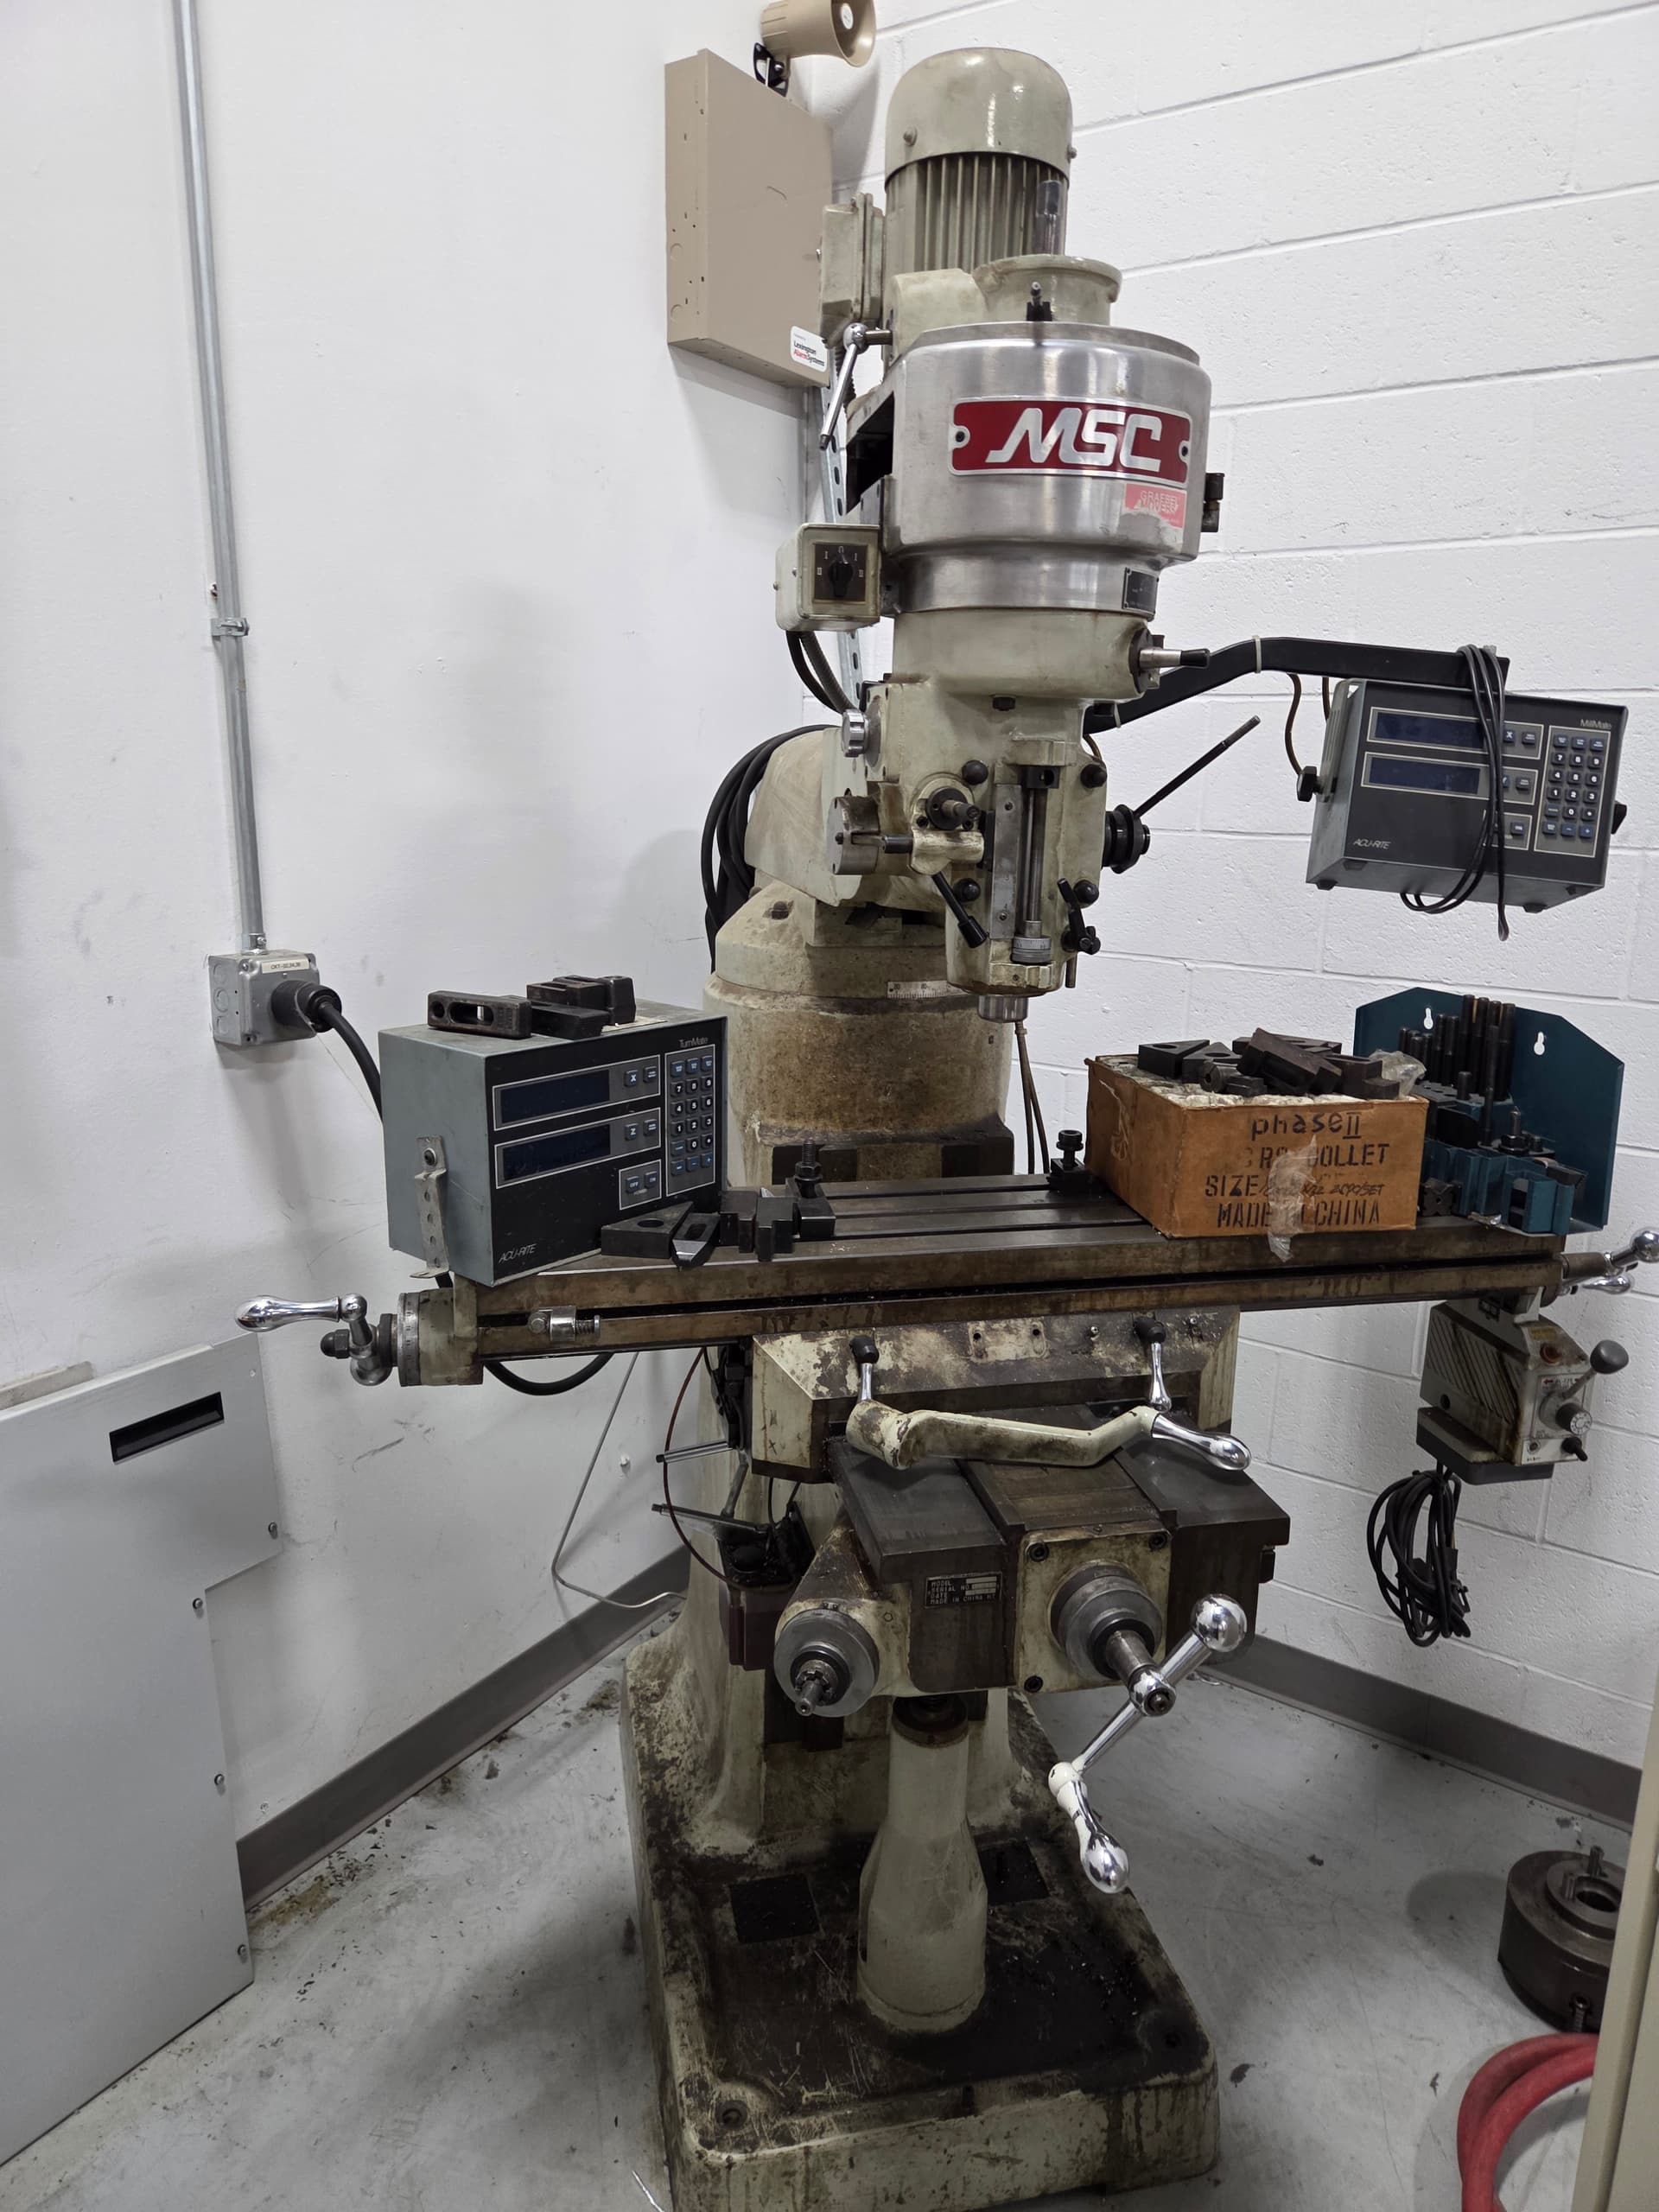
MSC Vertical Knee Mill
Wilmington, MA
Ends Tue, Oct 13, 10:00 AM CT
Lot 46
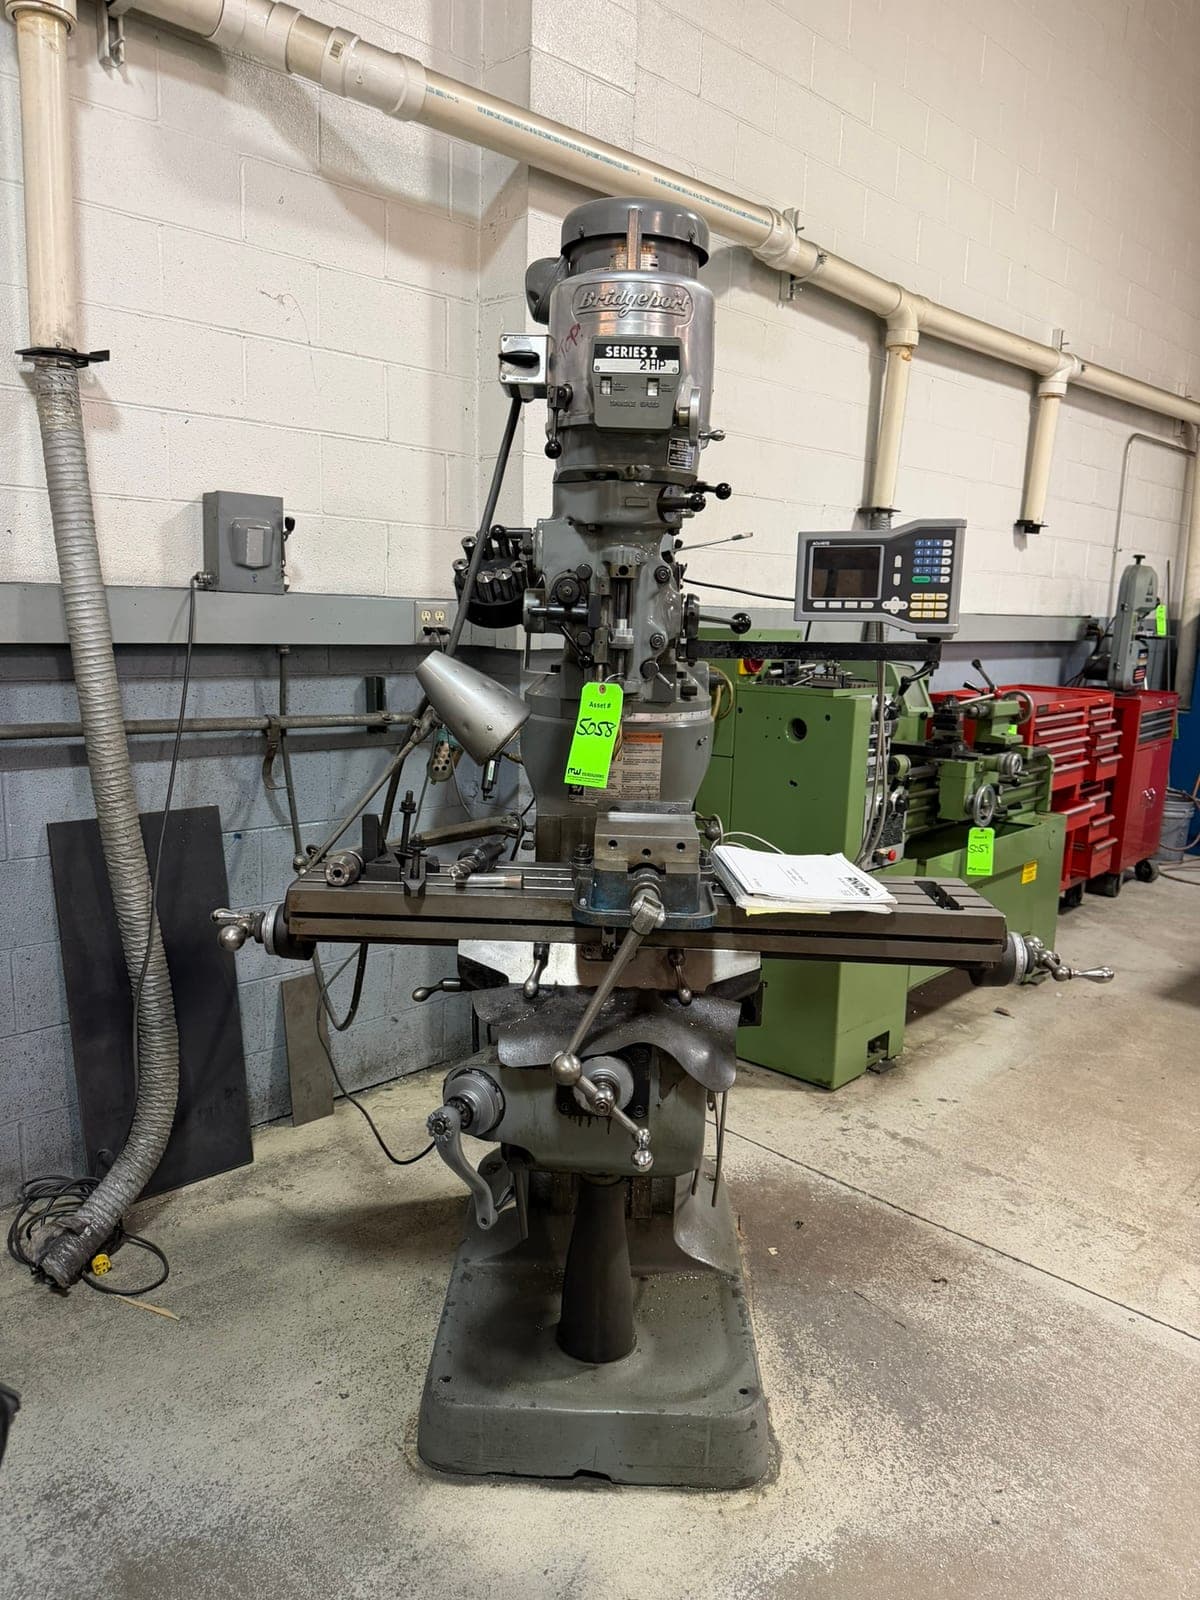
Bridgeport 2 HP Vertical Milling Machine
Naperville, IL
Live auction · Tue, Oct 27, 10:00 AM CT
Bridgeport Vertical Milling Machine
USA
Looking for Something Specific?
Most of our inventory sells before we can list it online. If you need a specific brand, model, or specification, tell us what you need—we have access to unlisted equipment and machines coming in from plant closures.
Looking to Sell?
Meadoworks is an active cash buyer of used industrial equipment. Get a free valuation from our AMEA-certified appraisers.
About Used Knee Mills
A knee mill raises and lowers the table on a knee, under a spindle that stays in the head. The operator dials a slot, a face or a hole by hand, or with a power feed on the table. It is the Bridgeport-shaped machine, and Hurco built them too. One machine in this group is a bed mill, with the table on a fixed bed rather than a knee. That is a different structure. Read the photo. A quill that drills and a head that nods are the knee-mill habits. A machining center with a tool changer is not this machine, even when the shop is still called a toolroom.
Travels are X and Y on the table and a quill or a knee for Z. A part that does not fit the table does not fit, and a knee that has lost its gibs will not hold a height. The spindle taper, often an R8 or a 30 or 40 taper, has to match the tooling you own. Speed comes from a belt, a vari-speed head or a gear range. Power is modest. This is for a fixture, a bracket or a second-op face, not for hogging a steel pocket all shift. A digital readout is the difference between counting handwheel turns and knowing where you are. A CNC knee, when the screws are motorized, is still a knee. It is not a vertical machining center with a changer and a full enclosure.
The ram, the turret and the knee ways are the wear. A loose ram nods under a cut and leaves a taper you will chase in the gibs. Quill bearings that rumble will not drill a round hole. Power feed that slips on X is a clutch or a screw. Nod the head, lock it, and indicate a vise before you believe the dials.
A used knee mill should be moved through its travels under power and by hand. Listen to the spindle at the top of the range. Rock the knee and the ram. Confirm the taper and whether a vise or a readout is still on the machine. Match the table to the part you actually fixture. A bed mill in the same offering is sized by its bed, not by a knee. Do not price them as the same iron. Ways that are smooth in the middle and tight at the ends have been used where every job lives.
How to Choose a Used Knee Mill
Manual vs CNC Knee Mill
A manual machine is right when a toolmaker is standing at the handles and the lot size is one or two. Power feeds help, and they do not make it a CNC. A CNC knee mill is right when you want a program on that same class of machine and you do not need a tool changer or a large enclosure.
The ways and the spindle still decide the cut. A tired manual machine with a control hung on it is not a sound CNC. Tram the head and feel the knee either way.
How to Size a Knee Mill
Size table travel to the part, quill travel to the holes and the bores, and spindle taper to the tooling you already own. Horsepower has to match the cutter, not a wish.
Knee travel sets the height under the spindle. A part that will not fit between the table and the head will not be saved by a longer program. Confirm the control, if there is one, still runs, and that the power is the voltage in your shop. Ways come before cosmetics. Measure the iron before you compare screens.
Knee Mill Specs to Compare
| Spec | Typical range | Why it matters |
|---|---|---|
| Table travel | The part has to fit the travels. A knee mill with a short table will not grow because the control is newer. | |
| Spindle taper | R8 on many manuals, steeper on heavier mills | Tooling has to fit the taper. An R8 shop and a 40-taper spindle are not a small adapter problem. |
| Quill travel | Quill travel is how deep you can go without moving the knee. A short quill limits boring. | |
| Knee travel | The knee sets capacity in Z for the part and the vise. Measure it with the vise you will use. | |
| Horsepower | A small spindle stalls in a heavy cut. Horsepower on the plate has to cover the work, not the paint. | |
| Control | Manual, power feed and CNC are different buys. A dead control on a CNC knee mill is a manual machine. |
Table travel
The part has to fit the travels. A knee mill with a short table will not grow because the control is newer.
Spindle taper
Typical range: R8 on many manuals, steeper on heavier mills
Tooling has to fit the taper. An R8 shop and a 40-taper spindle are not a small adapter problem.
Quill travel
Quill travel is how deep you can go without moving the knee. A short quill limits boring.
Knee travel
The knee sets capacity in Z for the part and the vise. Measure it with the vise you will use.
Horsepower
A small spindle stalls in a heavy cut. Horsepower on the plate has to cover the work, not the paint.
Control
Manual, power feed and CNC are different buys. A dead control on a CNC knee mill is a manual machine.
What to Inspect on a Used Knee Mill
Tram the head
The spindle should be square to the table. A head that will not tram cuts a taper you cannot program out.
Move the knee
The knee should lift smoothly and lock. Play in the knee is a tapered face on every part.
Feel the table ways
Gibs should adjust and the table should not rock. Scored ways are a rebuild, not a lube job.
Run the spindle
Listen through the speed range. A growl is bearings. A spindle that only turns by hand is not proven.
Check the quill
The quill should feed and return without a grab. A loose quill drills oversized holes.
Read the taper
Confirm R8 or the steeper taper against the tooling you own. Do not assume an adapter is in the drawer.
Power the control
On a CNC machine, the control should boot and move an axis. A dark screen is a project.
Meadoworks Track Record
12
Sold through Meadoworks
4
Listed now
Makes we have handled most
Common models
Bridgeport Series I, Bridgeport Series 1
Related Equipment
- Mills & Drills
The family of manual toolroom machines
- Drill Presses
Straight holes when a mill is more than you need
- Machining Centers
A VMC when the knee mill is too small
Knee Mills Brands We've Sold
Common Applications
Frequently Asked Questions
How do I size a knee mill for table travel?
The part, the vise and the travel in X and Y have to agree, with room to enter the cut. Quill travel covers drilling and boring depth. Knee travel covers the height under the spindle once the vise is on the table. Spindle taper has to match tooling you own, often R8 on a manual machine. Horsepower has to survive the cutter. A CNC knee mill adds a control, and it does not add travels the iron does not have. Measure the iron. Then decide manual or CNC.
What should I inspect on a used knee mill?
Tram the head, move the knee and feel the table for rock. Scored ways and a loose gib appear as a tapered cut. Run the spindle through the speeds and listen for bearings. The quill should feed without grabbing. Read the taper. On a CNC machine, boot the control and command an axis. A pretty paint job on a loose knee is the usual disappointment. Power feed, if it is there, should engage. A machine that only sits square in a photo has not been trammed.
Manual or CNC: which knee mill do I need?
Manual when a person is at the handles and the work is one-off or a short setup. Power feeds are still manual. CNC when you want that same knee-and-column machine to repeat a program and you do not need a tool changer or a large enclosure. A tired set of ways with a control bolted on is not a good CNC. Tram and the knee matter more than the badge on the screen.
How is a knee mill different from a VMC?
On a knee mill the knee carries the table up and down, and the head sits on a ram and a turret on the classic layout. A vertical machining center moves the head or the table in a fixed frame, usually with a tool changer and an enclosure. Travels, rigidity and tool capacity are in a different class. A knee mill is the toolroom and the short-run machine. Buying a knee mill for work that needs a tool changer and long axes will stall the job.
What spindle taper should a knee mill have?
The taper your tooling already fits. Many manual machines are R8. Heavier mills and some CNC knee mills use a steeper taper. An adapter can bridge a small gap and it adds stick-out and a joint you did not want in a finish cut. Read the spindle before you load the truck. Collets, end-mill holders and a boring head all have to match. A drawer full of R8 and a 40-taper spindle is a second purchase. The ways still matter after the taper is right.
When is a CNC knee mill enough instead of a machining center?
When the parts fit the table, the lot size does not need a tool changer, and the rigidity of a knee is enough for the cutter. Fixtures, one-offs and short repeats are the usual case. When the part is large, the cycle is long, or you need many tools in one setup, the machining center is the machine. A CNC the machine does not become a VMC because the control looks modern. Measure travels and look at the knee.
